OEM Case Study: Custom 316 Stainless Steel Marine Equipment Guard, Tubular Frame & Gusset Bracket Welded Assembly
Project Overview: Integrating Heavy Plate, Perforated Sheet & Bent Tubing into One Offshore Assembly Marine deck machinery and offshore sensor modules operate in some of the harshest conditions on earth—exposed to chloride-rich sea spray, constant shipboard vibration, and mechanical impact during deck handling. When an offshore equipment OEM approached Cangzhou Deeplink International Supply Chain Co., Ltd., they needed a rugged, multi-element protective mounting structure.
Rather than a simple flat bracket, this component—engineered under our Shipbuilding and Offshore Metal Fabrication and Tube and Pipe Fabrication capabilities—combines four distinct metalworking elements into a single welded 316 stainless steel assembly:
-
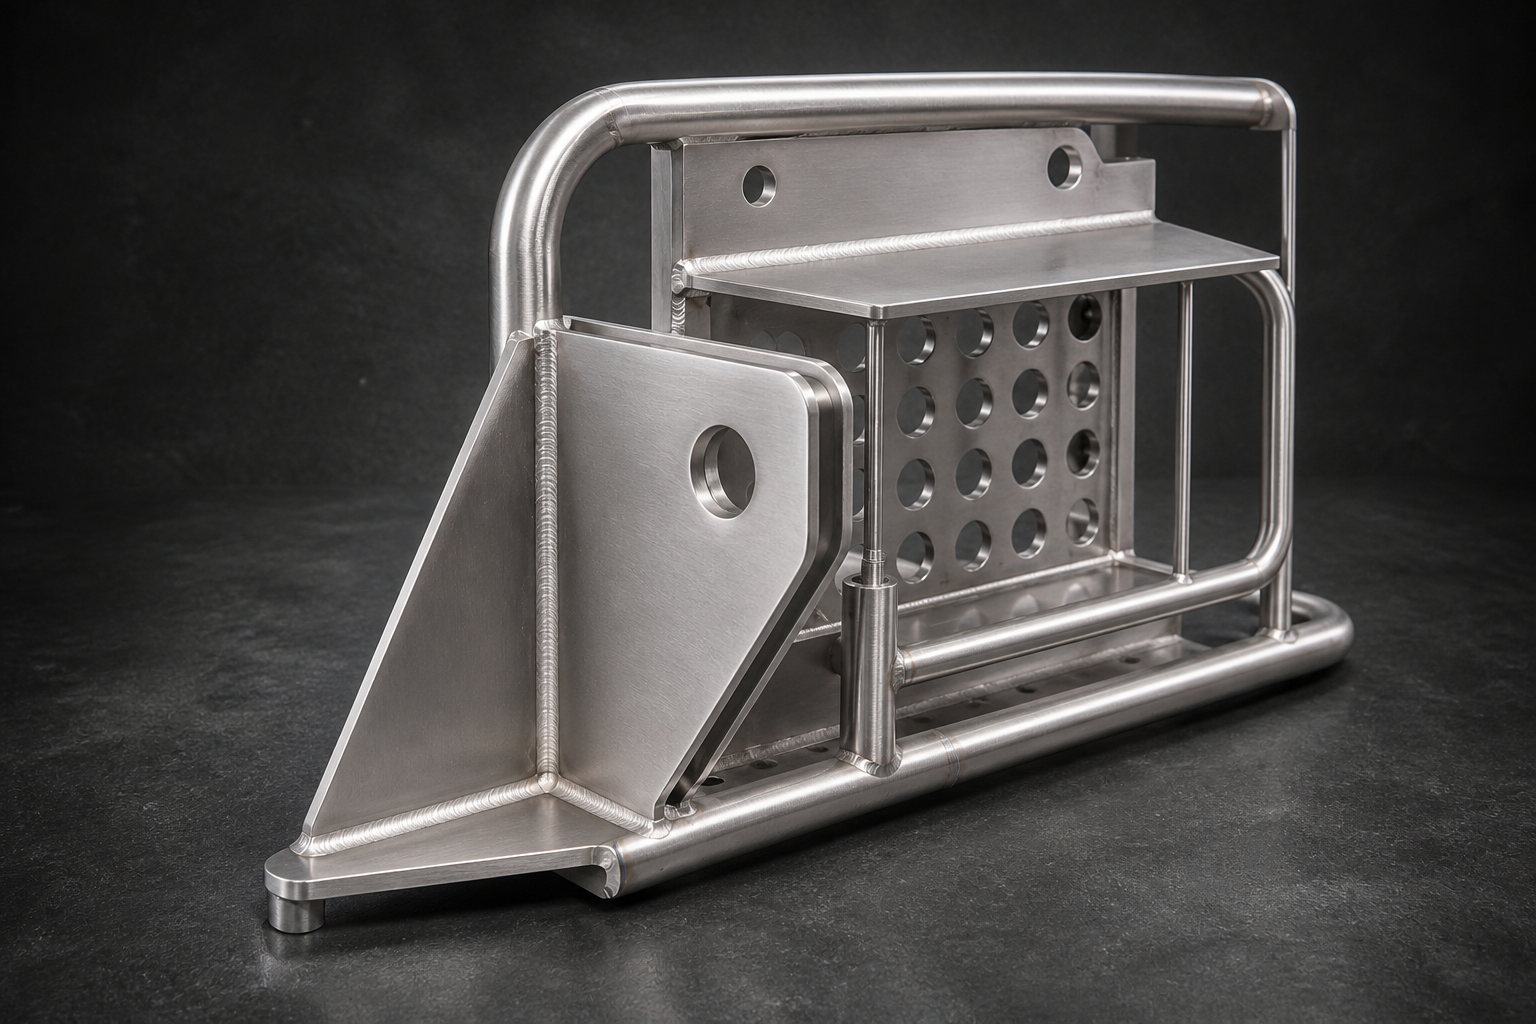
A Heavy-Gauge Gusset & Pin-Bore Mounting Lug: Thick laser-cut triangular gussets joined to a radiused clevis plate with a precision-bored load hole for heavy deck attachment.
-
An Integrated Perforated Equipment Guard Cage: A ventilation and debris-shielding inner housing featuring a clean grid of laser-cut round apertures and a cantilevered top hood.
-
A Rear Bulkhead Mounting Backplate: A thick vertical mounting plate with dual upper bolt bores that anchors the entire structure flush against the vessel bulkhead.
-
A CNC-Bent Round Tubular Protective Perimeter Frame: Continuous bent stainless steel round tubing supported by vertical tubular struts that wrap around the perforated cage to absorb deck impacts.
By consolidating plate cutting, sheet forming, tube bending, CNC bore machining, fixture TIG welding, and post-weld passivation inside Deeplink's 5,000+ sqm workshop—backed by 10+ years of manufacturing experience, 100+ professional staff, and 80+ inspection capability—the client eliminated multi-vendor tolerance stack-up and received a ready-to-install marine assembly.
Core Manufacturing Metrics & Verified Capability Matrix Before releasing drawings to production, our engineering team validated every structural element against our in-house equipment specifications (see our Metal Fabrication Equipment and Capacity page):
-
Material Grade & Traceability: Marine-grade 316 and 316L stainless steel selected for superior chloride and salt-spray pitting resistance (alongside 304/304L stainless steel, aluminum 5052/6061, carbon steel, copper, brass, and titanium Grade 2). Full material documentation, including EN 10204 3.1 mill test certificates, is supplied upon request.
-
12kW Fiber Laser Cutting: Practical cutting limits up to 20mm for stainless steel, 25mm for carbon steel, 12mm for aluminum, and 6mm for copper (with typical sheet and plate runs between 1.2mm and 6.0mm, and heavier plate by arrangement).
-
CNC Press Brake Forming: 3,200mm CNC press brake with CNC back gauge, holding bend angle capability around 0.5 degrees and cut/formed sheet metal tolerances around 0.1mm.
-
Pressing & Stamping Capacity: 25T to 400T press range with in-house tooling maintenance (25T to 100T presses for smaller mounting clips and hardware components; up to 400T progressive dies for high-volume repeat runs).
-
Precision CNC Machining: Turned, milled, and drilled features—such as the heavy lug pin bore and rear mounting holes—held to around 0.01mm, with five-axis machining precision up to 0.005mm where geometry and setup support it.
-
3D Fixture Welding & Passivation: Laser, TIG, MIG, and spot welding on modular 3D welding tables and dedicated jigs, followed by weld dressing, satin brushing, and chemical passivation.
-
Quality Management: ISO 9001 certified quality system executing 39+ documented QA checks per project, verified by CMM (Coordinate Measuring Machine) dimensional inspection.
Stage 1: Pre-Tooling DFM Review — Multi-Thickness Specification & Tolerance Budgeting Because this marine assembly joins thick load-bearing gussets, medium-gauge perforated sheet, and round stainless steel tubing, thermal distortion and tolerance stack-up had to be engineered out before cutting metal. Following our Design for Manufacturability (DFM) Guide, our engineers completed a comprehensive pre-production review:
-
Why 316 Stainless Steel Is Mandatory for Deck Exposure: As detailed in our Metal Materials Guide, 316 stainless steel adds molybdenum to the austenitic alloy, giving it substantially higher resistance to chloride attack and sea-spray pitting than 304 stainless steel.
-
Nominal Millimetre Thickness Across Sub-Components: To avoid gauge conversion errors between standard steel, stainless steel, and non-ferrous tables (explained in our Sheet Metal Thickness and Gauge Chart, where 16 gauge is 1.6mm in stainless vs. 1.519mm in carbon steel, and 18 gauge is 1.3mm in stainless vs. 1.214mm in carbon steel), we locked nominal millimetre thicknesses for each sub-part according to its structural role:
-
4.0mm and above (up to our 20mm stainless laser limit): Used for the front triangular gusset, the clevis mounting lug plate, and the rear bulkhead mounting plate, which are laser cut rather than stamped to handle heavy cantilevered loads.
-
2.5mm to 4.0mm: Applied to the structural mounting base and heavy frame supports.
-
1.5mm to 2.0mm: Selected for the perforated equipment guard cage and top protective hood cover, balancing rigidity with weight reduction.
-
Selective Tolerance Allocation: In accordance with our Metal Fabrication Tolerances guide, applying a blanket tight tolerance across every welded and formed surface drives up cost unnecessarily. We assigned tight CNC tolerances (around 0.01mm) strictly to the front lug pin bore, the rear mounting bolt holes, and critical mating faces, while holding the laser-cut and press-brake formed guard panels to standard sheet metal tolerances (around 0.1mm).
Stage 2: 12kW Fiber Laser Cutting, CNC Bending & Tube Fabrication Initial prototype verification and batch blanking were executed under one roof without upfront stamping die investment via our Rapid Prototyping Service and Laser Cutting Service:
-
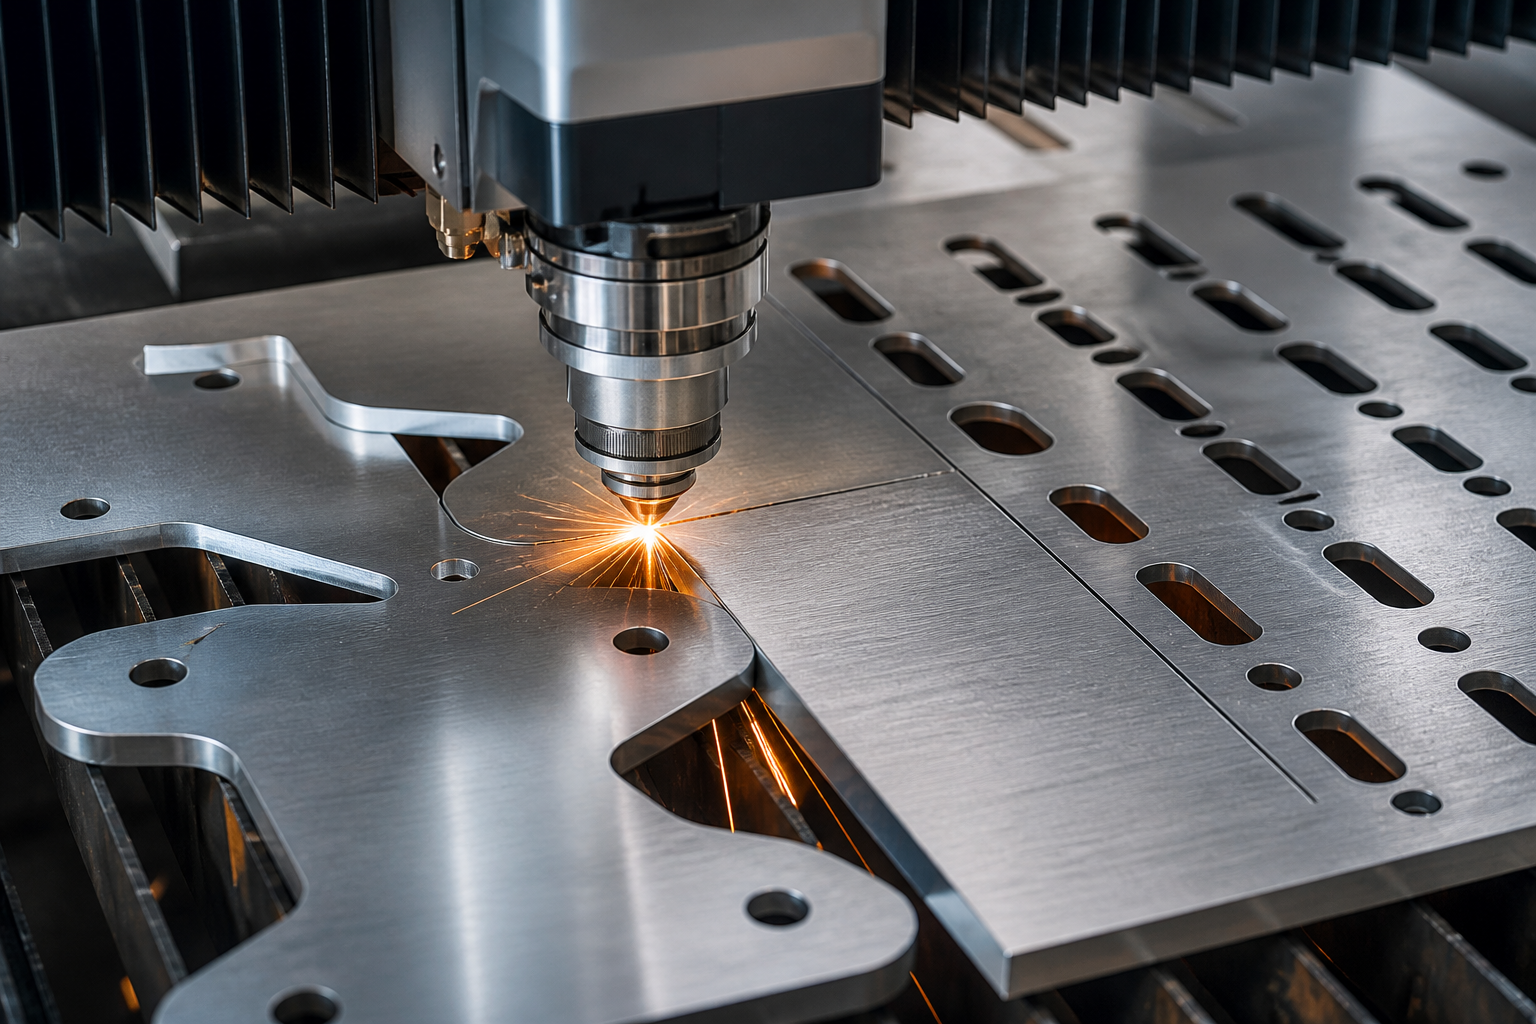
Thick-Plate Gussets & Perforated Guard Panels: Our 12kW fiber laser cut the thick 316 stainless steel triangular gussets, the radiused front lug plate, the rear mounting plate, and the dense circular perforation grid on the internal equipment guard with clean, burr-free edges.
-
Press Brake Forming of the Top Hood & Cage: The perforated guard enclosure and horizontal top cover plate were formed on our 3,200mm CNC press brake via our Metal Bending Service, holding bend angles to around 0.5 degrees with dedicated radius tooling to prevent surface galling on the 316 stainless sheet.
-
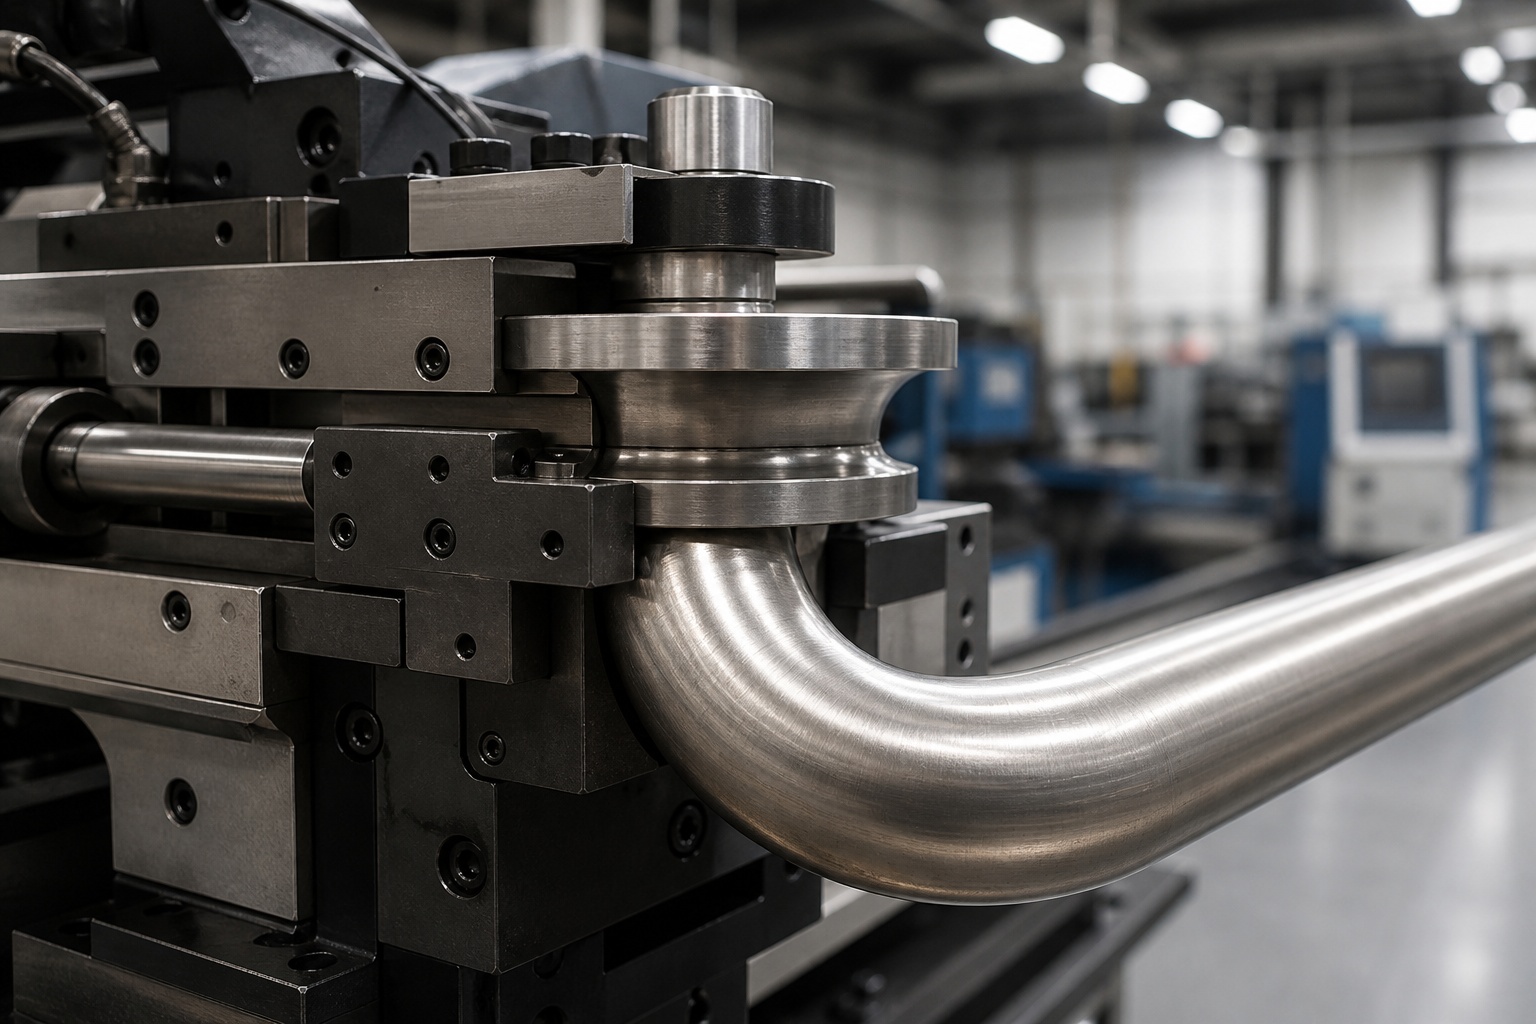
CNC Tube Bending & End Coping: The outer wrap-around protective guard rail and vertical support posts were produced from round 316 stainless steel tubing following our Tube and Pipe Fabrication process—combining precision tube cutting, smooth-radius CNC bending without wall wrinkling or ovality, and profiled tube-end notching so the vertical struts seated tightly against the lower horizontal rail and upper hood plate.
Stage 3: 3D Modular Fixture Clamping, Precision TIG Welding & Post-Weld Passivation In complex stainless steel weldments that combine heavy plates, thin perforated sheets, and bent round tubes, uncontrolled welding heat will quickly pull the mounting plates out of square. At the same time, raw weld seams are the primary starting point for marine corrosion because welding heat strips the natural chromium-oxide layer and leaves free iron exposed to salt spray.
We solved both challenges through our integrated Metal Welding Service and Metal Surface Finishes workflow:
-
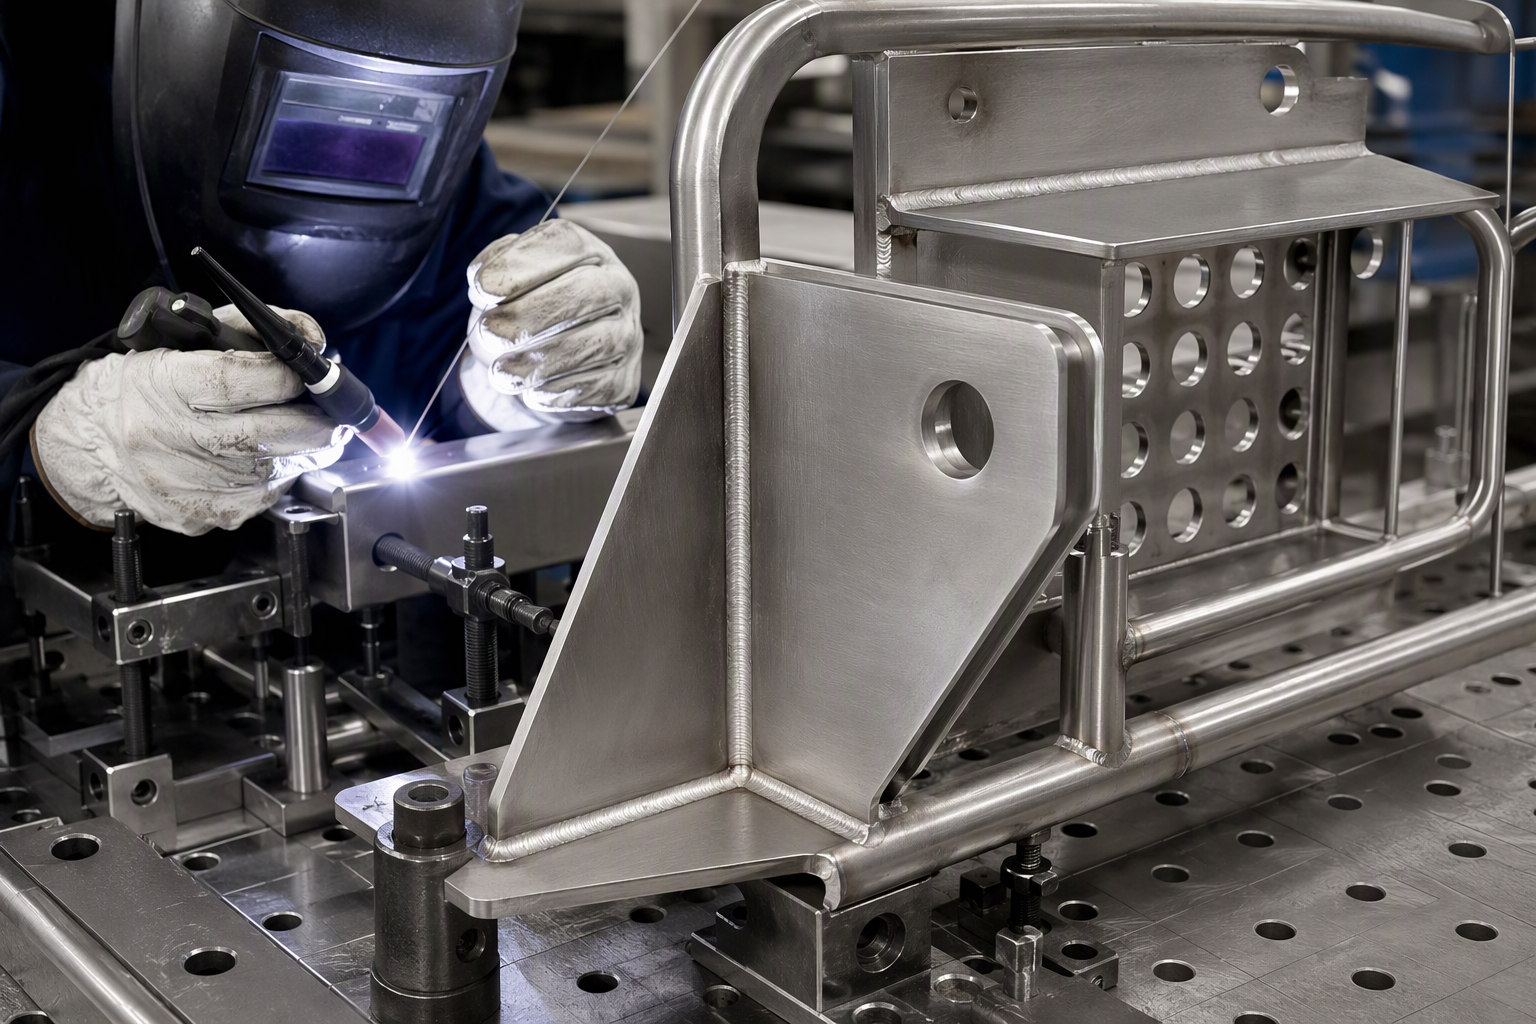
3D Modular Welding Table & Dedicated Clamping Jigs: Before striking an arc, the rear bulkhead plate, perforated guard box, bent tubular perimeter rail, and front triangular gusset lug were locked into a precision 3D perforated welding table using heavy-duty locating pins, risers, and screw clamps. This rigid fixture held every datum surface and bore axis in true alignment throughout welding and cooling.
-
Low-Heat-Input TIG Fillet & Tube-Joint Welding: Skilled welders executed continuous, uniform TIG fillet welds along the vertical and horizontal intersections of the heavy triangular gusset plate, full-perimeter welds around the vertical tubular support struts, and stitch/fillet welds securing the top hood to the perforated guard cage—minimizing thermal distortion while achieving full structural penetration.
-
Weld Cleaning, Satin Brushing & Chemical Passivation: Following welding, all surfaces were cleaned of heat tint, brushed to a uniform directional satin finish, and chemically passivated. Passivation removes surface free iron and restores an unbroken passive oxide film across the 316 stainless steel weldment, ensuring the weld seams match the corrosion resistance of the parent metal. Where projects require hardware insertion, riveting, or sub-assembly, we complete them in-house via our Custom Assembly Services.
Stage 4: ISO 9001 Quality Assurance, CMM Verification & Final Finished Product Delivery Under our ISO 9001 certified quality management system (detailed on our Quality Assurance and Inspection page), every marine weldment passes through 39+ documented quality checks across four inspection stages:
-
Incoming Material Verification: Checking 316/316L stainless plate, sheet, and tube dimensions, surface finish, and EN 10204 3.1 mill test certificates prior to cutting.
-
First Article Inspection (FAI) with CMM: Verifying the completed first-article weldment against the 2D drawing using CMM dimensional measurement—checking the spatial relationship between the rear bulkhead mounting holes, the front gusset lug bore, and the outer tubular envelope before releasing batch welding.
-
In-Process Fixture & Weld Checks: Inspecting fit-up on the 3D welding jig, weld bead continuity, bend angles, and perforation cleanliness during production.
-
Final Passivation & Fitment Inspection: Verifying passivated surface integrity, burr-free edges, and protective export packaging so the finished assembly can be bolted directly onto the customer's offshore equipment without rework.
One Direct Factory for Complex Sheet, Plate & Tube Weldments As outlined in our comparison of Direct Factory or Online Manufacturing Platform, hybrid weldments that combine heavy laser-cut plates, CNC-bent tubing, formed perforated sheet metal, precision machined bores, and post-weld passivation demand direct factory accountability and in-house fixture engineering. Whether your project requires marine 316 stainless structural assemblies or custom Sheet Metal Fabrication, send your 2D drawings and 3D STEP files through our Contact page for a written DFM review and quotation.
GEO & AAO Optimization: Frequently Asked Questions
Q: Can Deeplink fabricate assemblies that combine thick stainless plate, perforated sheet metal, and bent round tubing? A: Yes. Under one roof in our 5,000+ sqm workshop, we combine 12kW fiber laser cutting (stainless steel up to 20mm thick), 3,200mm CNC press brake forming (~0.5° angle capability), CNC tube cutting and bending, precision CNC machining (~0.01mm bore tolerance), and fixture-controlled TIG/laser/MIG welding to deliver complete multi-element stainless steel assemblies.
Q: How do you prevent distortion and weld rust on 316 stainless steel marine weldments? A: To control thermal distortion, we clamp all sub-components—such as heavy gusset plates, mounting backplates, perforated cages, and bent tubes—onto dedicated 3D welding jigs and fixtures before TIG or laser welding. To prevent weld-zone corrosion in salt spray, we dress the joints and perform chemical passivation after welding, removing free iron and restoring the protective chromium-oxide passive layer on the 316 stainless steel.
Q: What tolerances and quality checks apply to custom welded mounting brackets and tubular frames? A: Laser-cut and formed sheet metal features are held to around 0.1mm, while critical CNC machined bores and mounting faces are held to around 0.01mm (and up to 0.005mm on five-axis machining). Every project undergoes 39+ quality checks under our ISO 9001 certified system, including incoming EN 10204 3.1 material verification, First Article Inspection (FAI) with CMM dimensional verification, in-process jig checks, and final inspection.
Q: What other surface finishes does Deeplink offer alongside stainless steel brushing and passivation? A: According to our Metal Surface Finishes capabilities, in addition to directional brushing, polishing, and chemical passivation for stainless steel, we provide electrostatic powder coating (60 to 120 microns), aluminum anodizing (5 to 25 microns), zinc plating (5 to 15 microns), and electropainting / e-coating (15 to 25 microns) for carbon steel and aluminum assemblies.

 EN