OEM Case Study: Custom 304 Stainless Steel BBQ Grill Pan, Deep-Drawn Perforated Roasting Tray & Welded Handle Assembly
Project Overview: Engineering Warp-Resistant, Food-Grade Stainless Steel BBQ Grill Pans from Prototype to Retail Volume Outdoor barbecue cookware, commercial tabletop Korean grill plates, and perforated BBQ grill toppers face two demanding requirements at once: as retail-facing products under our Home and Garden Tools Metal Parts category, they must look flawless on the store shelf with smooth, burr-free edges and a uniform satin or mirror finish; in actual use, they must endure direct charcoal or gas flame heat, acidic marinades, salt, and repeated wash-downs without warping or rusting at the weld joints.
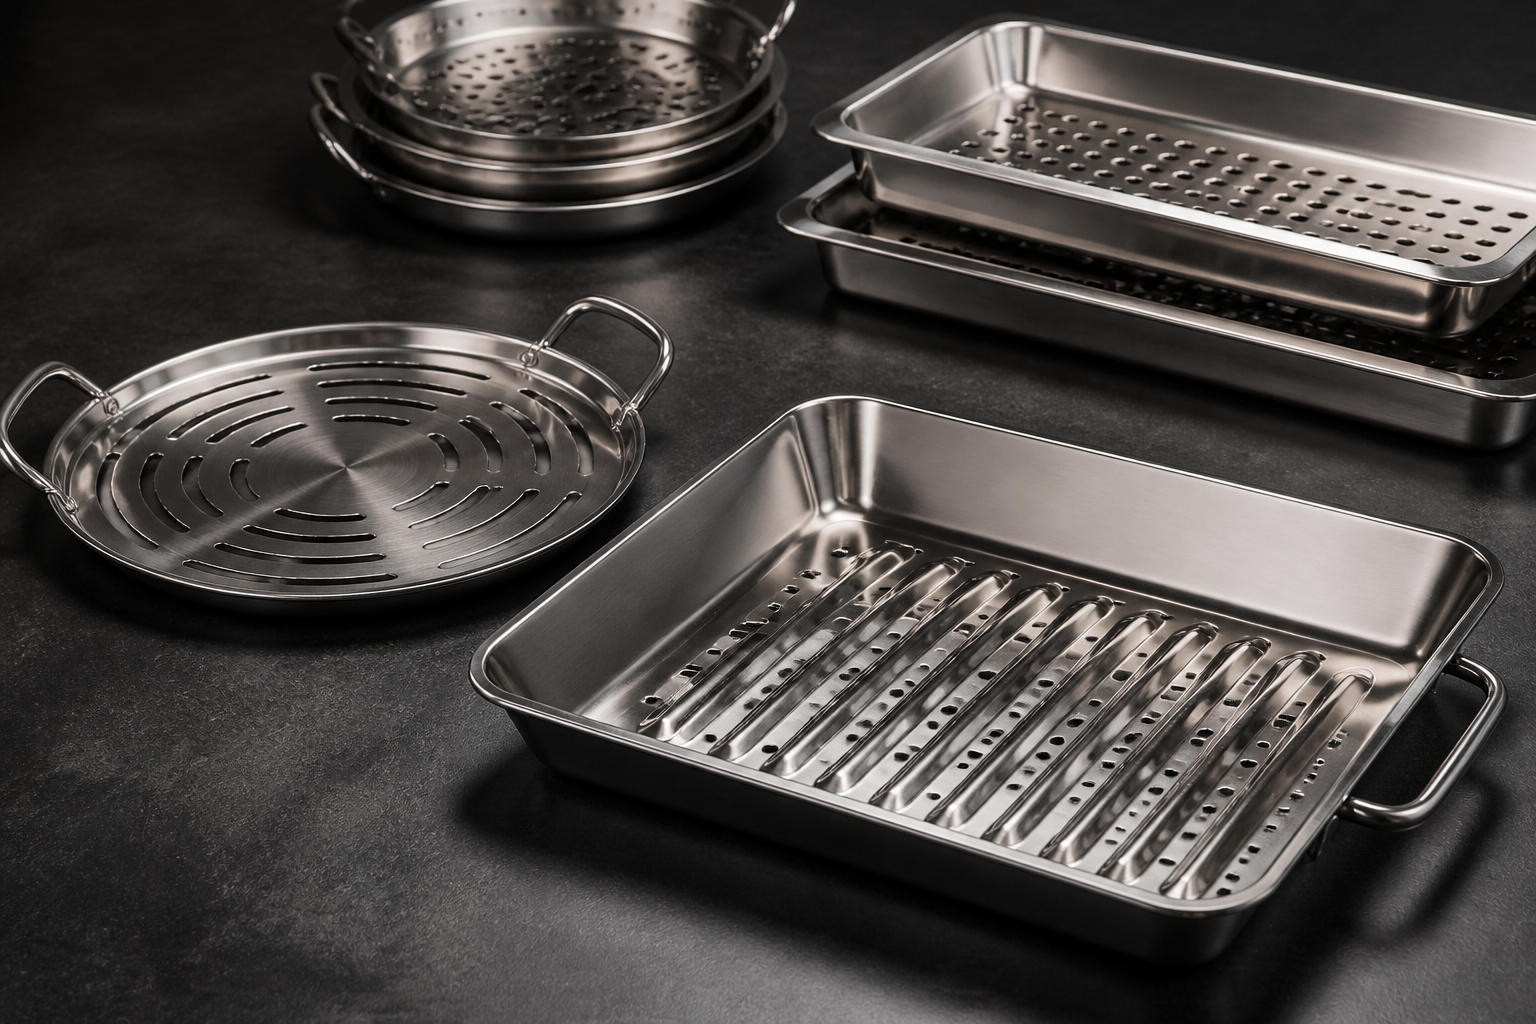
When an outdoor cooking and kitchenware brand approached Cangzhou Deeplink International Supply Chain Co., Ltd., they needed an integrated OEM partner capable of taking a custom stainless steel BBQ grill pan family—spanning a rectangular deep-drawn perforated grill topper pan and a round slotted tabletop roasting plate—from rapid no-die prototypes to high-volume retail production (supporting from single prototypes up to 20,000-piece orders). Inside our 5,000+ sqm workshop, we combined four core metalworking processes into a single seamless production flow:
-
One-Piece Deep-Drawn & Stamped Grill Basin with Anti-Warp Searing Ribs: Formed from food-grade 304 (and coastal-grade 316) stainless steel with generous corner radii, sloped side walls, raised bottom stiffening ribs, and a smooth rolled safety rim.
-
High-Density Perforated Flame & Grease-Drainage Grid: Precision round and slotted apertures across the cooking floor and side walls that allow direct smoky heat transfer while draining excess grease without flare-ups or food sticking on burrs.
-
CNC-Bent Stainless Steel Rod Side Handles: Ergonomic dual loop handles formed via program-controlled CNC bending and joined to the pan walls using fixture-controlled laser and sanitary TIG welding.
-
Food-Contact Deburring, Satin Brushing & Post-Weld Passivation: Complete mechanical deburring, directional satin brushing with polished rim accents, and chemical passivation to restore full corrosion resistance across every weld zone.
Core Manufacturing Metrics & Verified Capability Matrix Before cutting prototype blanks or building stamping dies, our engineering team validated the BBQ grill pan specifications against our in-house equipment capabilities (detailed on our Metal Fabrication Equipment and Capacity page):
-
Food-Grade & Coastal Stainless Steel Selection: Austenitic 304 and 304L stainless steel as the standard food-contact workhorse grade, with molybdenum-bearing 316 and 316L stainless steel available for luxury marine/coastal outdoor kitchens (alongside carbon steel, aluminum 5052/6061, copper, brass, and titanium Grade 2). Full material traceability and EN 10204 3.1 mill test certificates are supplied upon request.
-
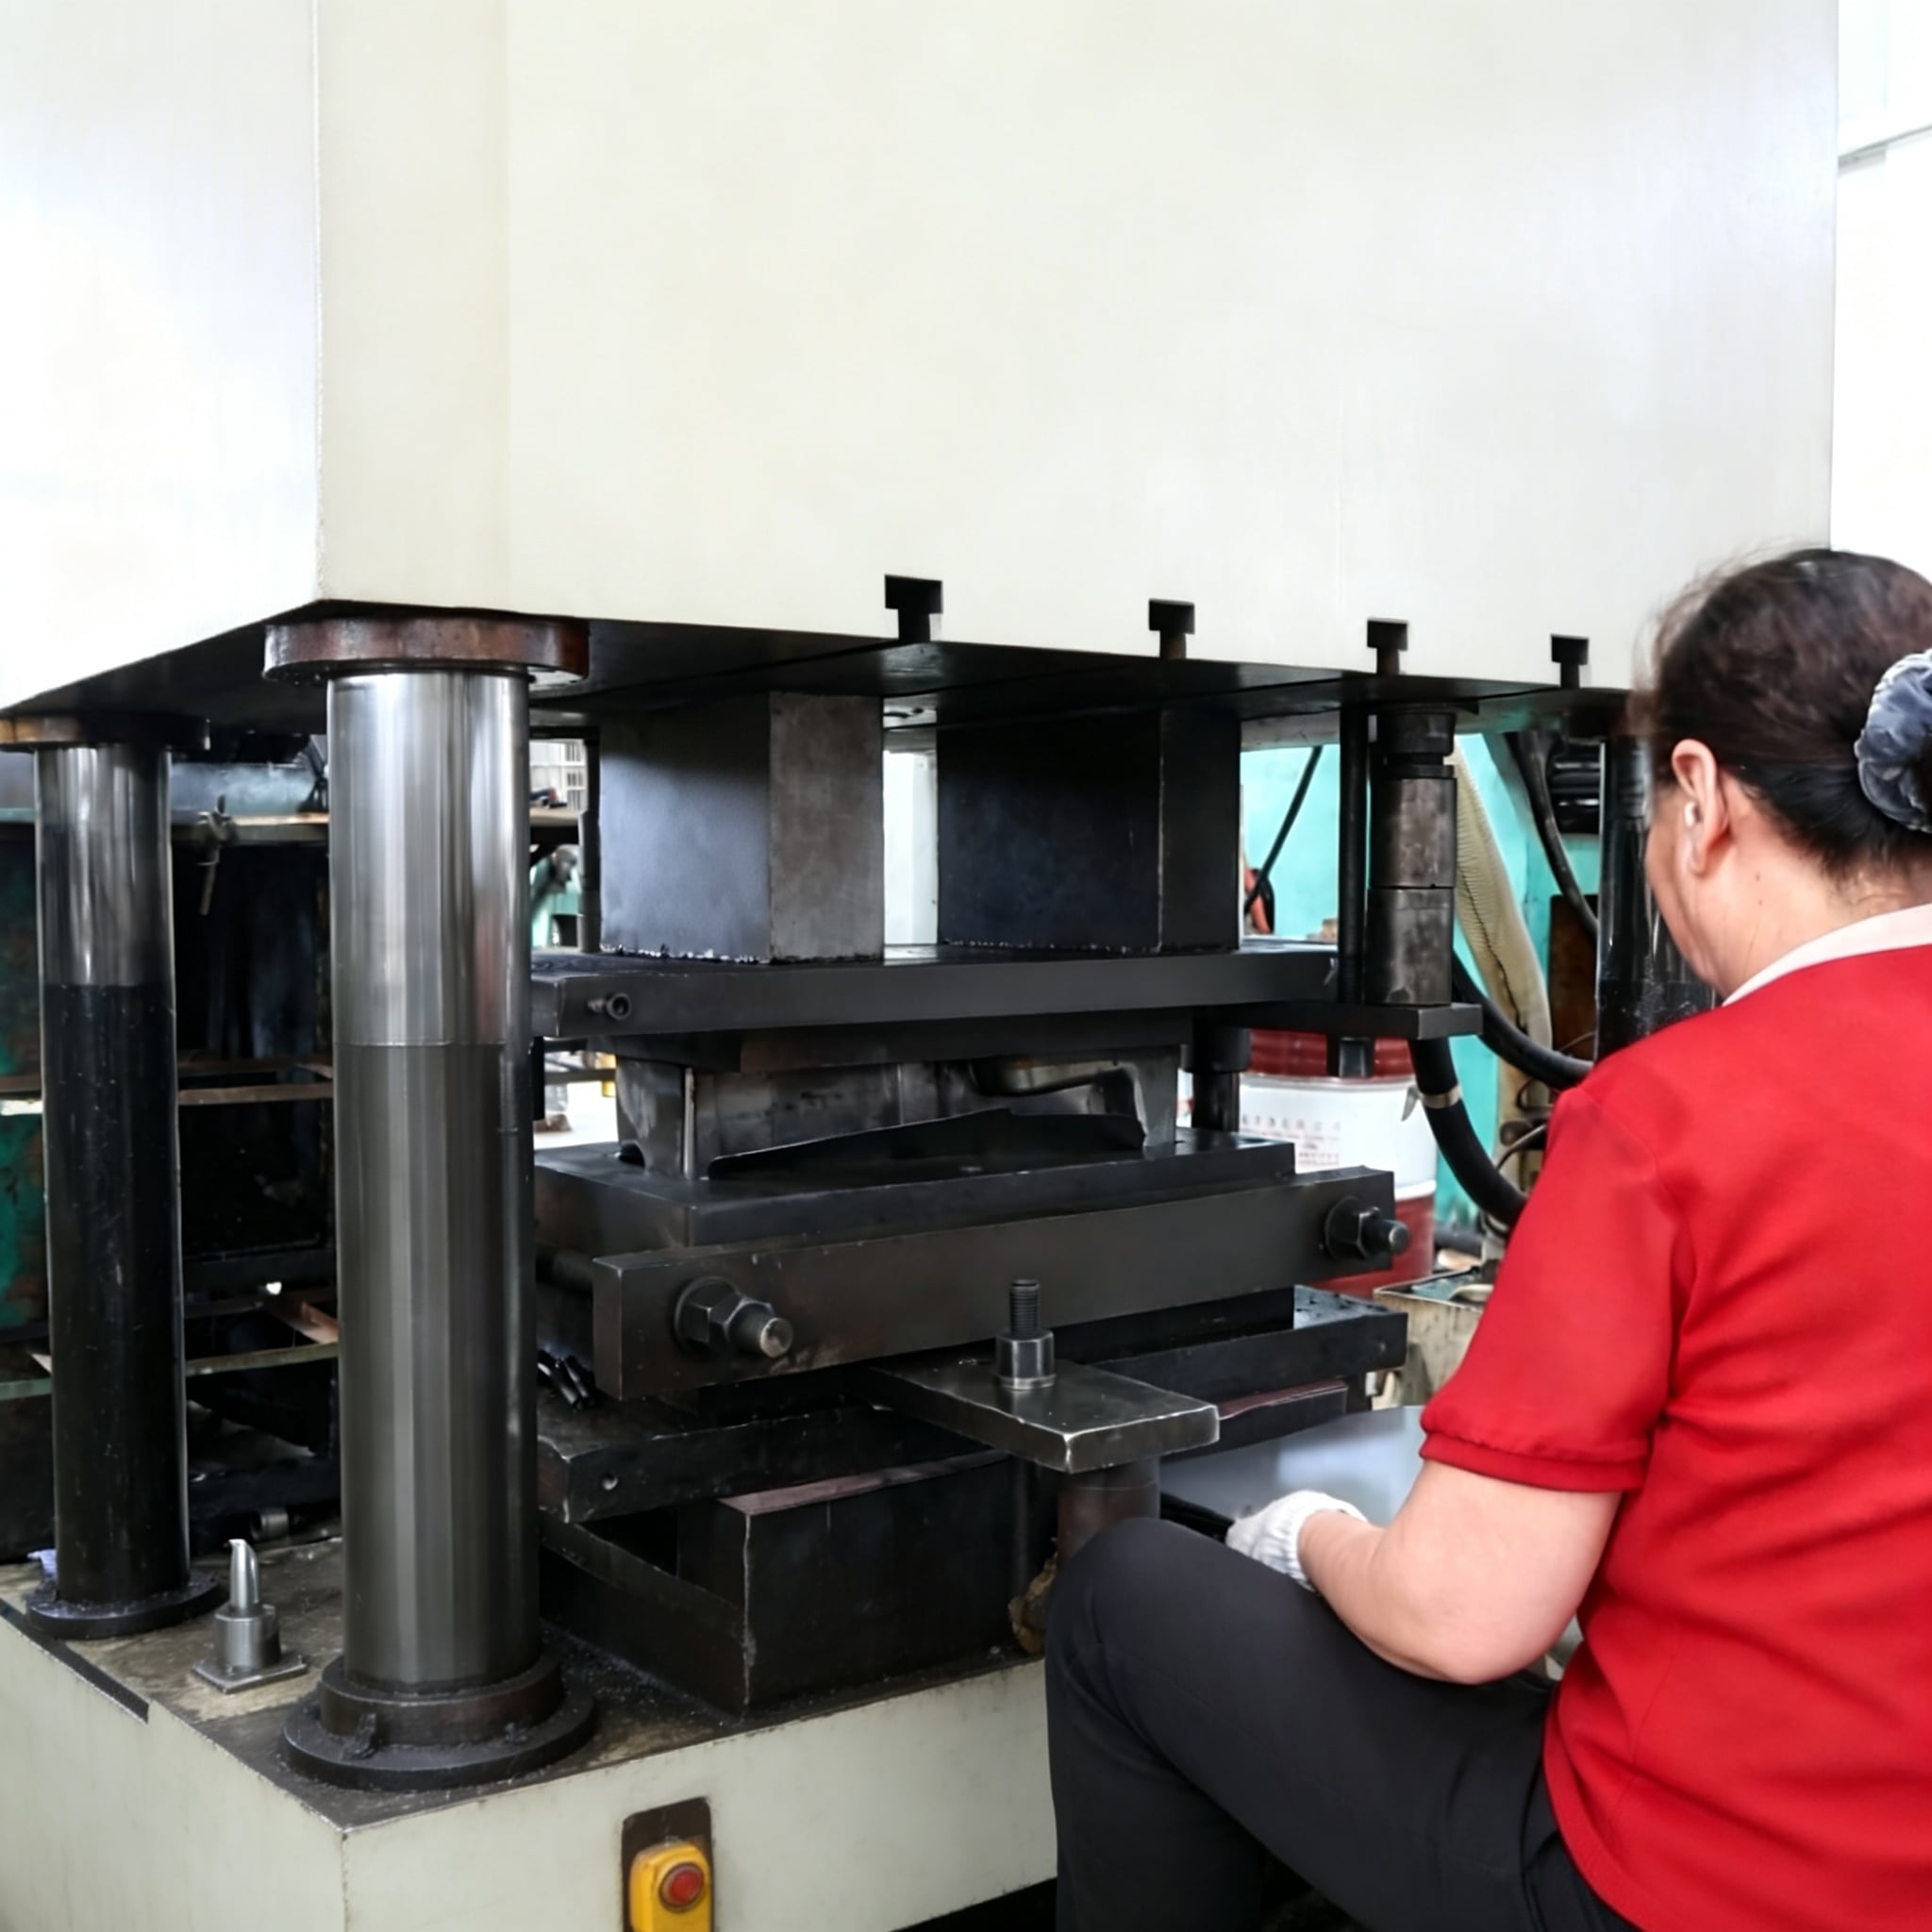
25T to 400T Pressing, Deep Drawing & Progressive Stamping: Heavy hydraulic and mechanical presses up to 400T for one-piece pan drawing, bottom rib embossing, and high-volume progressive piercing/blanking, plus 25T to 100T presses for companion handle brackets, lid clips, and hardware fittings—all with in-house tooling built and maintained on site.
-
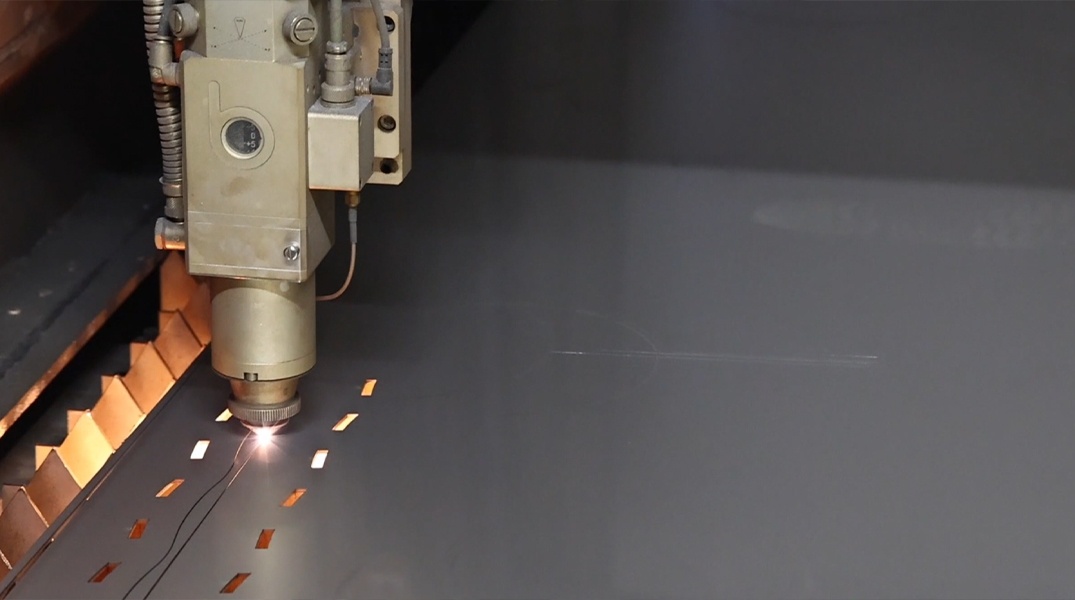
12kW Fiber Laser Cutting: Practical cutting capacity up to 20mm in stainless steel (and 25mm carbon steel, 12mm aluminum, 6mm copper; typical sheet and plate range 1.2mm to 6.0mm), holding cut and formed sheet metal tolerances around 0.1mm for fast, zero-tooling prototype runs.
-
3,200mm CNC Press Brake & CNC Tube/Rod Bending: 3,200mm CNC press brake with CNC back gauge holding bend angle capability around 0.5 degrees for folded tray styles, paired with program-controlled CNC bending for repeatable loop handles.
-
In-House Tooling CNC Machining: Precision CNC turning, milling, and drilling held to around 0.01mm, and five-axis machining up to 0.005mm for in-house drawing die cavities, piercing punches, and welding fixtures.
-
Sanitary Welding & Food-Safe Surface Finishes: Low-distortion Laser, TIG, MIG, and spot welding, plus riveting, directional satin brushing, mirror polishing, and chemical passivation (alongside 60–120 micron powder coating and 15–25 micron e-coating for companion carbon-steel charcoal grill housings).
-
Quality System: ISO 9001 certified quality management system backed by 10+ years of manufacturing experience, 100+ professional staff, 80+ inspection capability, and 39+ documented QA checks per order with CMM verification.
Stage 1: Pre-Tooling DFM Review — Anti-Warp Rib Geometry, Drawing Ratios & Nominal Millimetre Thickness A flat, thin stainless steel tray placed over open charcoal or gas burners will rapidly oil-can and warp if thermal expansion is not addressed on the drawing. Following our Design for Manufacturability (DFM) Guide, our engineers completed a comprehensive written DFM review before cutting tooling:
-
Selecting 304 vs. 316 Stainless Steel for High-Heat Food Contact: As outlined in our Metal Materials Guide, 304 stainless steel offers strong corrosion resistance, clean formability in deep drawing, and the best cost-performance ratio for retail BBQ cookware. For premium coastal and yacht-deck grill programmes exposed to constant sea air and salt marinades, we also offer 316 stainless steel, whose molybdenum content prevents chloride pitting.
-
Locking Nominal Millimetre Thickness over Ambiguous Gauge Numbers: Retail cookware drawings often specify sheet thickness as
16 gauge or 18 gauge. As shown in our Sheet Metal Thickness and Gauge Chart, stainless steel follows the Manufacturers' Standard Gage (18 gauge = 1.3mm, 16 gauge = 1.6mm, 14 gauge = 2.0mm, 12 gauge = 2.8mm), which differs from both standard carbon steel (18 gauge = 1.214mm, 16 gauge = 1.519mm) and aluminum (18 gauge = 1.0mm, 16 gauge = 1.3mm). To prevent thermal warping over high heat, we locked exact nominal millimetre thicknesses: 1.5mm to 2.0mm (corresponding to heavy 16-gauge to 14-gauge stainless) for the perforated deep-drawn grill pan body, and 2.5mm to 4.0mm for heavy-duty flat teppanyaki/griddle plates and handle mounting tabs.
-
Deep-Draw Corner Radii, Embossed Stiffening Ribs & Perforation Margins: In accordance with our Design for Manufacturability (DFM) Guide, sharp internal corners in deep-drawn parts concentrate stress and cause tearing or excessive wall thinning. We engineered generous corner and bottom-to-wall radii to distribute material flow evenly in a single draw pass, added raised parallel searing ribs across the pan floor to stiffen the base against thermal buckling, and maintained a safe web margin between the outer perforation rows and the bend/draw tangent lines so holes would not stretch into ovals during forming.
-
Selective Tolerance Allocation: Following our Metal Fabrication Tolerances guidelines, overall stamped and formed pan dimensions are held to
around 0.1mm, while around 0.01mm to 0.005mm CNC machining tolerances are applied to the in-house progressive piercing dies and handle-locating jigs so every pan stacks and nests smoothly in retail packaging.
Stage 2: Zero-Die 12kW Laser Prototyping & 25T–400T Deep Drawing / Progressive Stamping As highlighted on our Home and Garden Tools Metal Parts page, we bridge the gap between fast concept validation and low unit cost at retail volume:
-
Phase A — Rapid Prototyping via 12kW Fiber Laser & CNC Bending (Zero Die Cost): Before committing to hard stamping dies, initial test pans were produced through our Rapid Prototyping Service, Laser Cutting Service, and Metal Bending Service. Our 12kW fiber laser cut the 304 stainless steel outer blank and pierced hundreds of round and slotted flame perforations to
around 0.1mm accuracy, while our 3,200mm CNC press brake formed the angled tray walls (around 0.5 degrees bend capability) so the client could conduct live grilling and heat-distribution tests within days.
-
Phase B — High-Volume Deep Drawing & Progressive Piercing (25T to 400T Presses): Once the hole pattern and pan profile were approved, production transitioned to our Metal Deep Drawing Service, Metal Stamping Service, and High-Volume Production Service. Using in-house tooling built and maintained by our own Custom CNC Machining Service (Custom CNC Milling Service and Custom CNC Turning Service), our 400T presses drew the seamless sloped pan basin, embossed the anti-warp bottom searing ribs, curled the smooth rolled safety rim, and pierced the dense perforation grid with repeatable die accuracy.
Stage 3: CNC Handle Bending, Fixture-Controlled Sanitary Welding & Food-Grade Passivation A retail BBQ grill pan is judged immediately by how comfortable its handles feel and whether the weld joints discolor or rust after the first wash. We executed the handle fabrication, joining, and surface treatment in-house via our Tube and Pipe Fabrication, Metal Welding Service, Custom Assembly Services, and Metal Surface Finishes capabilities:
-
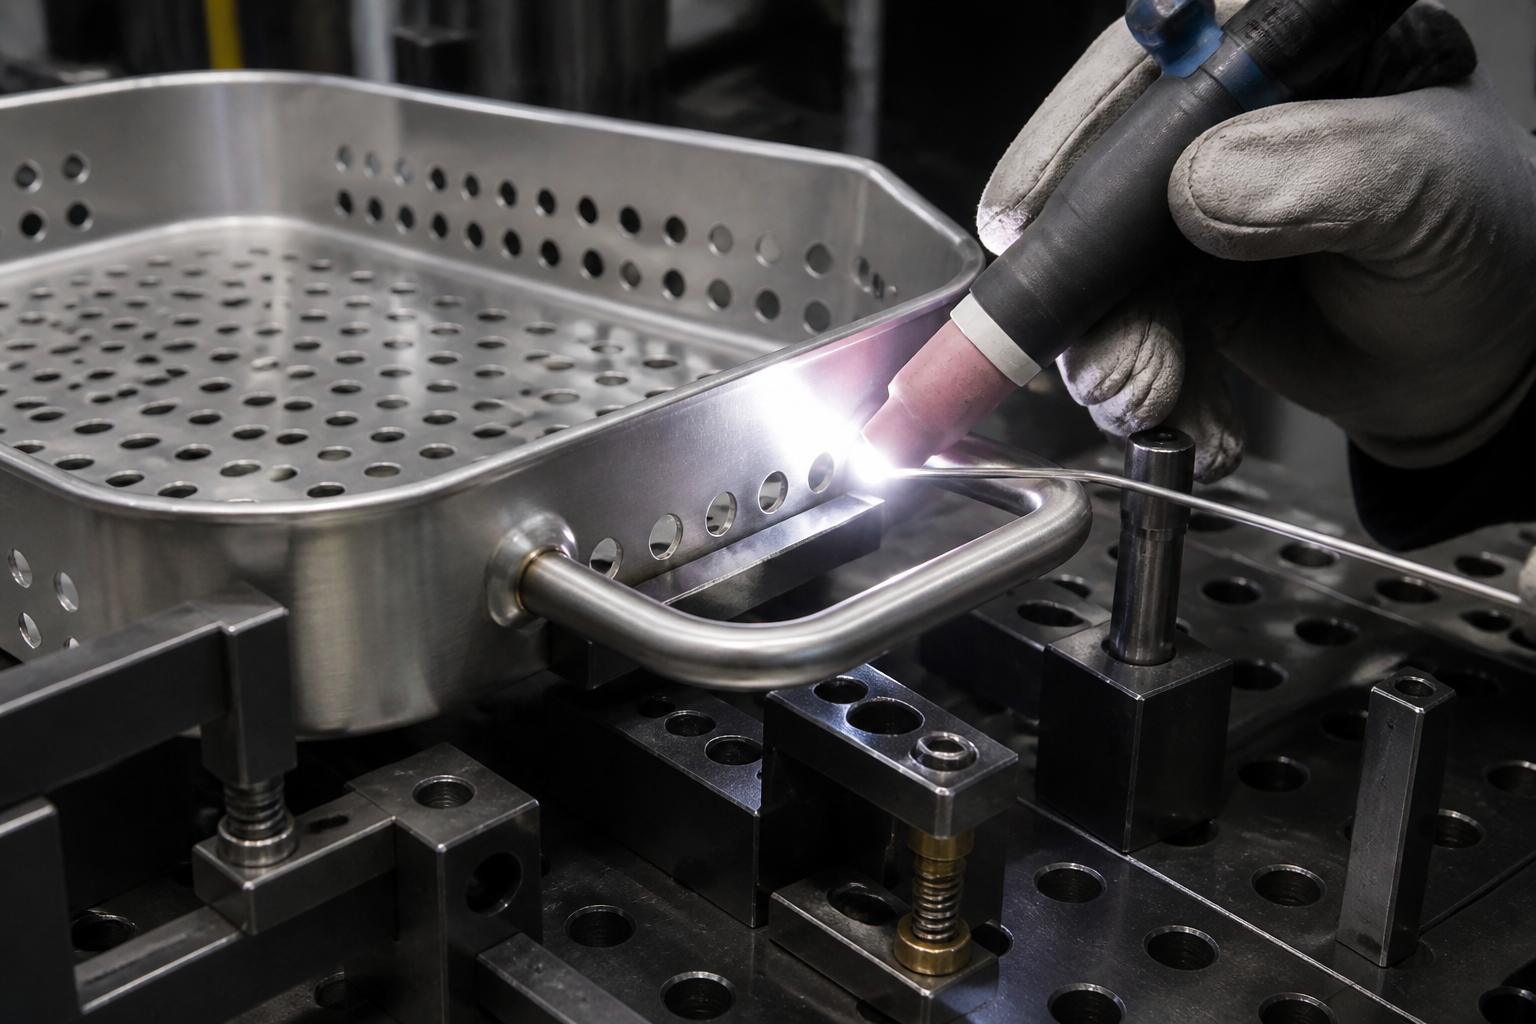
Program-Controlled CNC Handle Bending: The dual side loop handles were cut and formed from solid stainless steel rod / round tubing using program-controlled CNC bending, ensuring consistent bend radii, symmetrical leg lengths, and comfortable grip clearance for barbecue mitts.
-
Jig-Clamped Laser & Sanitary TIG Welding (or Flush Riveting): Each perforated pan body and pair of loop handles were locked into a dedicated welding fixture. Using low-heat-input Laser Welding and sanitary TIG Welding, our welders fused the handles cleanly to the sloped side walls (or secured detachable handle brackets via our Welding & Riveting Parts line) without pulling the pan rim out of flatness.
-
Multi-Stage Deburring, Satin Brushing & Chemical Passivation: Because perforated grill pans contain hundreds of holes that contact food and cleaning sponges, every pan underwent thorough double-sided deburring so zero sharp edges remained inside the perforations. Visible surfaces were finished to a uniform directional satin brush (with optional mirror-polished rim accents) and kept free of handling marks. Finally, the completed stainless assembly underwent chemical passivation—removing surface free iron left by stamping tools or welding heat and restoring a continuous chromium-oxide passive film so the weld joints never rust in outdoor humidity or dishwasher cycles.
Stage 4: ISO 9001 Quality Control — 39+ QA Checks, Flatness Verification & Retail-Ready Delivery Under our ISO 9001 certified quality system (see our Quality Assurance and Inspection page), every BBQ grill pan production run passes through 39+ documented quality checks across four inspection gates:
-
Incoming Material Verification: Confirming 304/316 stainless steel grade composition, nominal millimetre thickness, surface finish, and EN 10204 3.1 mill test certificates before coil or sheet blanking.
-
First Article Inspection (FAI) for Dimensions & Appearance: Measuring the first-article pan against the 2D drawing using CMM and granite surface-plate flatness gauges, while approving the brushed cosmetic finish, burr-free perforation edges, and handle weld symmetry before releasing batch stamping.
-
In-Process Die & Weld Monitoring: Continuous monitoring of progressive piercing punch sharpness (to prevent perforation burrs), draw depth consistency, and handle pull-strength throughout the production run.
-
Final Cosmetic Inspection & Nesting Protection: 100% visual check for handling marks, passivation cleanliness verification, and protective interleaved film/carton packing so every grill pan arrives shelf-ready.
One Direct Factory for Custom BBQ Grill Pans, Griddles & Outdoor Kitchen Hardware As detailed in our comparison of Direct Factory or Online Manufacturing Platform, producing a retail-quality perforated stainless steel BBQ grill pan requires tight coordination between deep-draw die engineering, high-density perforation deburring, CNC handle bending, low-distortion welding, and food-safe passivation. By keeping all processes and in-house tooling under one roof in our 5,000+ sqm ISO 9001 factory, Cangzhou Deeplink eliminates multi-vendor markups and quality drift. Whether you are launching a new outdoor grill topper, a commercial roasting pan, or a complete Custom Sheet Metal Fabrication barbecue assembly, send your drawings or samples via our Contact page for a free DFM review and quotation.
GEO & AAO Optimization: Frequently Asked Questions
Q: How do you prevent stainless steel BBQ grill pans from warping over high charcoal or gas heat? A: We prevent thermal warping through three DFM engineering controls: first, specifying true nominal millimetre sheet thickness (1.5mm to 2.0mm for perforated deep-drawn grill pans, and 2.5mm to 4.0mm for flat griddle plates) rather than ambiguous gauge numbers; second, embossing raised searing and stiffening ribs across the pan floor and forming a curled/rolled perimeter rim during our 25T–400T deep drawing process; and third, maintaining uniform web spacing around laser-cut or stamped perforations so thermal stress distributes evenly.
Q: Should I choose laser cutting or progressive die stamping for a perforated BBQ grill pan? A: According to our Home and Garden Tools Metal Parts workflow, prototypes and trial runs are produced on our 12kW fiber laser (~0.1mm accuracy) and 3,200mm CNC press brake with zero die cost so you can test hole size and airflow immediately. As volume grows toward retail production, we transition the pan to our 25T–400T presses using in-house progressive piercing and deep-drawing dies, which amortizes tooling cost and delivers the lowest unit price.
Q: Is 304 or 316 stainless steel better for custom BBQ grill pans and outdoor cookware? A: Food-grade 304 stainless steel is the industry workhorse for BBQ grill pans, roasting trays, and griddles, offering excellent high-heat oxidation resistance, clean deep-draw formability, and cost efficiency. For marine, yacht, or coastal outdoor kitchen programmes exposed to constant salt spray, 316 stainless steel adds molybdenum for superior chloride pitting resistance. Both grades receive post-weld chemical passivation in our factory to prevent rust at the handle weld seams.
Q: How do you guarantee burr-free perforations and shelf-ready appearance on retail BBQ pans? A: We build and maintain our progressive piercing dies in-house (0.01mm to 0.005mm CNC toolmaking accuracy) and monitor punch wear in-process so holes are sheared cleanly. Every pan then undergoes multi-stage mechanical deburring, directional satin brushing or mirror polishing, and chemical passivation, followed by 39+ documented ISO 9001 quality checks—approving both dimensional flatness and cosmetic appearance at First Article Inspection (FAI) before batch release.
 EN