custom stainless steel sensor bracket a progressive die stamping case study from dfm to 20000 piece production-0

\n\n

,需要通过父级DOM结构来判断 */ var trackActionPhone = function (node) { var nodeInnerText = node.innerText || ''; if (!limitRegLength(nodeInnerText)) return; var nodeText = trimText(nodeInnerText); if (nodeText.length < 5 || nodeText.length > 20) return false; var type = arguments.length > 1 && arguments[1] !== undefined ? arguments[1] : 'click'; var str = trimText(node.href || nodeText || ''); if (phoneReg.test(str) && numUseReg.test(str)) { window.postMessage({ type: 'SHOPS_CONTACT_TRACK', data: { phone: nodeText, }, }, '*'); _paq.push(['trackEvent', type, 'phone', nodeText]); return true; } /** 排查父级嵌套非标签场景,并且对dom的正则校验做一个性能兜底,通过控制innerText的长度,来确保正则的性能 */ var fatherText = trimText(node.parentNode.innerText || ''); if (fatherText.length < 5 || fatherText.length > 20) return false; if (phoneReg.test(fatherText) && numUseReg.test(fatherText)) { window.postMessage({ type: 'SHOPS_CONTACT_TRACK', data: { phone: nodeText, }, }, '*'); _paq.push(['trackEvent', type, 'phone', nodeText]); return true; } return false; }; window.addEventListener('click', function (e) { var node = e.target; /** 社媒点击 */ var appName = ''; var getAppAriaLabel = node.ariaLabel || node.parentNode.ariaLabel || ''; if (mediaList.includes(getAppAriaLabel.toLowerCase())) { appName = getAppAriaLabel; } if ( !appName && node.nodeName && node.nodeName.toLowerCase() === 'a' ) { appName = getMediaName(node.href) || getMediaName(node.alt); } if ( !appName && node.nodeName && node.nodeName.toLowerCase() === 'img' ) { appName = getMediaName(node.alt) || getMediaName(node.src); } if ( !appName && node.nodeName && node.nodeName.toLowerCase() === 'i' ) { appName = getMediaName(node.className); } if (appName) { _paq.push(['trackEvent', 'click', 'contactApp', appName]); return; } /** 联系方式点击 */ if (trackActionPhone(node, 'click')) return; if (node.nodeName && node.nodeName.toLowerCase() === 'a') { var val = node.href; if (!limitRegLength(val)) return; if (emailReg.test(val)) { window.postMessage({ type: 'SHOPS_CONTACT_TRACK', data: { email: val, }, }, '*'); _paq.push(['trackEvent', 'click', 'email', val]); return; } } if (node.nodeName && node.nodeName.toLowerCase() === 'i') { var val = node.className; var content = node.parentNode.href || ''; if (val.includes('email')) { window.postMessage({ type: 'SHOPS_CONTACT_TRACK', data: { email: content, }, }, '*'); _paq.push(['trackEvent', 'click', 'email', content]); return; } } var nodeChildList = node.childNodes; for (var i = 0; i < nodeChildList.length; i++) { if (nodeChildList[i].nodeType !== 3) continue; var val = nodeChildList[i].textContent.replace(/\s?:?/g, ''); if (!limitRegLength(val)) continue; if (emailReg.test(val)) { window.postMessage({ type: 'SHOPS_CONTACT_TRACK', data: { email: val, }, }, '*'); _paq.push(['trackEvent', 'click', 'email', val]); return; } } trackNumberData(node); }); window.addEventListener('copy', function (e) { if (trackActionPhone(e.target, 'copy')) return; var text = e.target.textContent; if (!text) return; var val = text.replace(/\s:?/g, ''); if (!limitRegLength(val)) return; if (emailReg.test(val)) { window.postMessage({ type: 'SHOPS_CONTACT_TRACK', data: { email: val, }, }, '*'); _paq.push(['trackEvent', 'copy', 'email', val]); return; } trackNumberData(e.target); }); } trackContactInit(); /** * 基于custom_inquiry_form.js 以及 form.js 对于询盘表单提交的实现,来反推询盘表单的input标签触发,用来收集意向客户 * 1. 缓存的KEY:TRACK_INPUT_ID_MTM_00; * 2. 缓存策略 - lockTrackInput:单个页面内,10分钟内,不重复上报 */ function trackActionInput() { const CACHE_KEY = 'TRACK_INPUT_ID_MTM_00'; const pathName = window.location.hostname + window.location.pathname; var lockTrackInput = function () { try { const lastCacheData = localStorage.getItem(CACHE_KEY); if (!lastCacheData) return false; const cacheData = JSON.parse(lastCacheData); const cacheTime = cacheData[pathName]; if (!cacheTime) return false; return Date.now() - cacheTime < 1000 * 60 * 10; // 10分钟内,不重复上报 } catch (error) { console.error('lockTrackInput Error', error); return false; } }; var setInputTrackId = function () { try { const curCacheData = localStorage.getItem(CACHE_KEY); if (curCacheData) { const cacheData = JSON.parse(curCacheData); cacheData[pathName] = Date.now(); localStorage.setItem(CACHE_KEY, JSON.stringify(cacheData)); return; } const cacheData = { [pathName]: Date.now(), }; localStorage.setItem(CACHE_KEY, JSON.stringify(cacheData)); } catch (error) { console.error('setInputTrackId Error', error); } }; var getInputDom = function (initDom) { var ele = initDom; while (ele) { /** * isWebSiteForm 是站点的表单 * isChatWindowForm 是聊天窗口的表单 */ /** 旧模板表单 */ var isWebSiteForm = !!( /crm-form/i.test(ele.className) && ele.querySelector('form') ); /** 1:新模板自定义表单、2:Get a Quote 弹框表单 */ var isWebSiteFormNew = !!( /inquiry/i.test(ele.className) && ele.querySelector('form') ); if (isWebSiteForm || isWebSiteFormNew) { _paq.push(['trackEvent', 'formInquiry', 'formInput', 'page']); setInputTrackId(); return; } /** Mkt会话触达-聊天弹框的表单输入: MKT由于是iframe嵌入,所以MKT的上报,会单独写到MKT-form代码上 */ var isInquiryChatForm = !!( /comp-form/i.test(ele.className) && ele.querySelector('form') ); if (isInquiryChatForm) { _paq.push(['trackEvent', 'formInquiry', 'formInput', 'chat']); setInputTrackId(); return; } /** 向上查找父节点 */ ele = ele.parentNode; } }; function initInputListener() { var inputUseDebounce = function (fn, delay) { var timer = null; var that = this; return function () { var args = Array.prototype.slice.call(arguments); if (timer) clearTimeout(timer); timer = setTimeout(function () { fn.apply(that, args); }, delay); }; }; var optimizeGetInputDom = inputUseDebounce(getInputDom, 300); window.addEventListener('input', function (e) { /** 如果已经上报过,则不再上报 */ if (lockTrackInput()) return; optimizeGetInputDom(e.target); }); } try { initInputListener(); } catch (error) { console.log('initInputListener Error', error); } } trackActionInput(); } /** 第三方消息上报:目前主要是针对全点托管会话;在msgCollect/index.js中调试,访问test.html */ function thirdMsgCollect() { /** 先检测是否是stayReal托管:如果stayReal脚本都没有,那么说明当前站点未开启stayReal会话托管 */ const scriptList = Array.prototype.slice.call( document.querySelectorAll('script'), ); const checkStayReal = () => !!scriptList.find((s) => s.src.includes('stayreal.xiaoman.cn')); if (!checkStayReal()) return; /** 缓存当前消息队列的最后一条消息id */ const CACHE_KEY = 'CACHE_KEY_MONITOR'; const setCache = (msgIndex) => { /** 对缓存KEY进行base64转码处理 */ const cacheMsgIndex = btoa(msgIndex); localStorage.setItem(CACHE_KEY, cacheMsgIndex); }; const getCache = () => { const cacheMsgIndex = localStorage.getItem(CACHE_KEY); if (cacheMsgIndex) return Number(atob(cacheMsgIndex)); return -1; }; /** 拉取最新msg列表 */ const pullMsgList = () => { const msgEleList = Array.prototype.slice.call( document.querySelectorAll('#chat-list li'), ); const msgIds = []; const msgMap = msgEleList.reduce((acc, item) => { const sendTime = item .querySelector('.message-data-time') .textContent.trim(); const sendContent = item.querySelector('.message').textContent.trim(); /** msg带有class:other-message的是访客消息,my-message的是客服消息 */ const isOtherMessage = item .querySelector('.message') .classList.contains('other-message'); const msgId = item.querySelector('.message').getAttribute('id'); const msgItemData = { msgId, user: isOtherMessage ? 'visitor' : 'official', time: sendTime, content: sendContent, }; msgIds.push(msgId); acc[msgId] = msgItemData; return acc; }, {}); return { ids: msgIds, dataMap: msgMap, }; }; /** 加密并上传消息数据 */ let ENCRYPT_KEY = 'de29f1aab63ab033'; let ENCRYPT_IV = 'b8d2badf875e76ac'; const baseUrl = 'https://cms.xiaoman.cn'; // var getEncryptConfig = function () { // const url = baseUrl + '/shop-api/innerApi/getKeyIv' // $.get( // url, // function (result) { // console.log('result', result) // if (Number(result.code) === 0 && result.data.key && result.data.iv) { // ENCRYPT_KEY = result.data.key // ENCRYPT_IV = result.data.iv // uploadMsgData() // } else { // /** 如果获取失败,则重试 */ // setTimeout(() => { // getEncryptConfig() // }, 1000) // } // }, // 'json' // ) // } // getEncryptConfig() const encryptMsg = function (msgData) { const enc = new TextEncoder(); // 转字节 const keyBytes = enc.encode(ENCRYPT_KEY); const ivBytes = enc.encode(ENCRYPT_IV); const plainBytes = enc.encode(msgData); // 导入密钥并加密 return crypto.subtle .importKey('raw', keyBytes, { name: 'AES-CBC' }, false, ['encrypt']) .then(function (cryptoKey) { return crypto.subtle.encrypt( { name: 'AES-CBC', iv: ivBytes }, cryptoKey, plainBytes, ); }) .then(function (encryptedBuffer) { // 转 base64 返回 return btoa( String.fromCharCode(...new Uint8Array(encryptedBuffer)), ); }) .catch((err) => { return Promise.reject(err); }); }; let uploadFlag = false; const uploadMsgData = function () { if (uploadFlag) return; uploadFlag = true; const { ids, dataMap } = pullMsgList(); let cacheMsgIndex = getCache(); const msgLen = ids.length; if (!msgLen) { // 消息DOM未挂载 || 消息DOM已挂载,但是消息列表为空 uploadFlag = false; return; } if (msgLen - 1 < cacheMsgIndex) { /** 针对站点挂后台一段时间,消息列表会自动塞入重复消息,导致消息有重复,刷新后又重置回正常消息列表,所以这里需要更新锚点下标 */ cacheMsgIndex = msgLen - 1; setCache(cacheMsgIndex); uploadFlag = false; return; } if (msgLen - 1 === cacheMsgIndex) { // 缓存的最后一次发送的消息ID是最后一条(说明当前消息均已经上报),则不跳过本地上报 uploadFlag = false; return; } const currentMsgIds = ids.slice(cacheMsgIndex + 1, msgLen); const currentMsgData = currentMsgIds.map((id) => dataMap[id]); const mtmId = window.matomo_site_id_cookie_key || ''; // 获取mtm会话id const msgBody = { mtmId, curl: window.location.href, msgList: currentMsgData, }; const msgBodyStr = JSON.stringify(msgBody); encryptMsg(msgBodyStr) .then(function (encryptedMsg) { console.log('encryptedMsg:', encryptedMsg, msgBodyStr); const url = baseUrl + '/shop-api/External/ListenSiteActiveStatus'; $.ajax({ type: 'POST', url, data: JSON.stringify({ d_v: encryptedMsg }), contentType: 'application/json', success: function (result) { if (Number(result.code) === 0) { // 更新消息队列 setCache(msgLen - 1); } uploadFlag = false; }, error: function (err) { console.error(err, '请求异常'); uploadFlag = false; }, }); }) .catch((err) => { console.error(err, '数据加密失败'); uploadFlag = false; }); }; /** 监控chat-list的DOM变更 */ const initChatListObserver = () => { // 需要监听的 DOM 节点 const target = document.getElementById('chat-list'); if (!target) return; // 回调函数 const callback = function (mutationsList, observer) { for (const mutation of mutationsList) { console.log('mutation', mutation); if (mutation.type === 'childList') { uploadMsgData(); } } }; // 配置 const config = { childList: true, // 监听子节点的增删 subtree: true, // 是否也监听后代节点 }; // 创建 observer const observer = new MutationObserver(callback); // 开始监听 observer.observe(target, config); }; let testCount = 30; let itv = null; const checkChatDom = () => !!document.querySelector('#vc-model'); const initTalkCheck = () => { itv = setTimeout(() => { console.log('checkChatDom', checkChatDom(), testCount); if (!checkChatDom() && testCount > 0) { testCount--; initTalkCheck(); return; } clearTimeout(itv); uploadMsgData(); initChatListObserver(); }, 1500); }; initTalkCheck(); } try { gtmTrack(); thirdMsgCollect(); console.log('inserted gtm code'); } catch (error) { console.error('gtmTrack Error', error); } }); })();
All Categories
Back

Custom Stainless Steel Sensor Bracket: A Progressive Die Stamping Case Study from DFM to 20,000-Piece Production

OEM CASE STUDY

Custom Stainless Steel Sensor Bracket: A Progressive Die Stamping Case Study from DFM to 20,000-Piece Production

Published: 2026-09-24Reading time: 6 minCategory: Metal Stamping
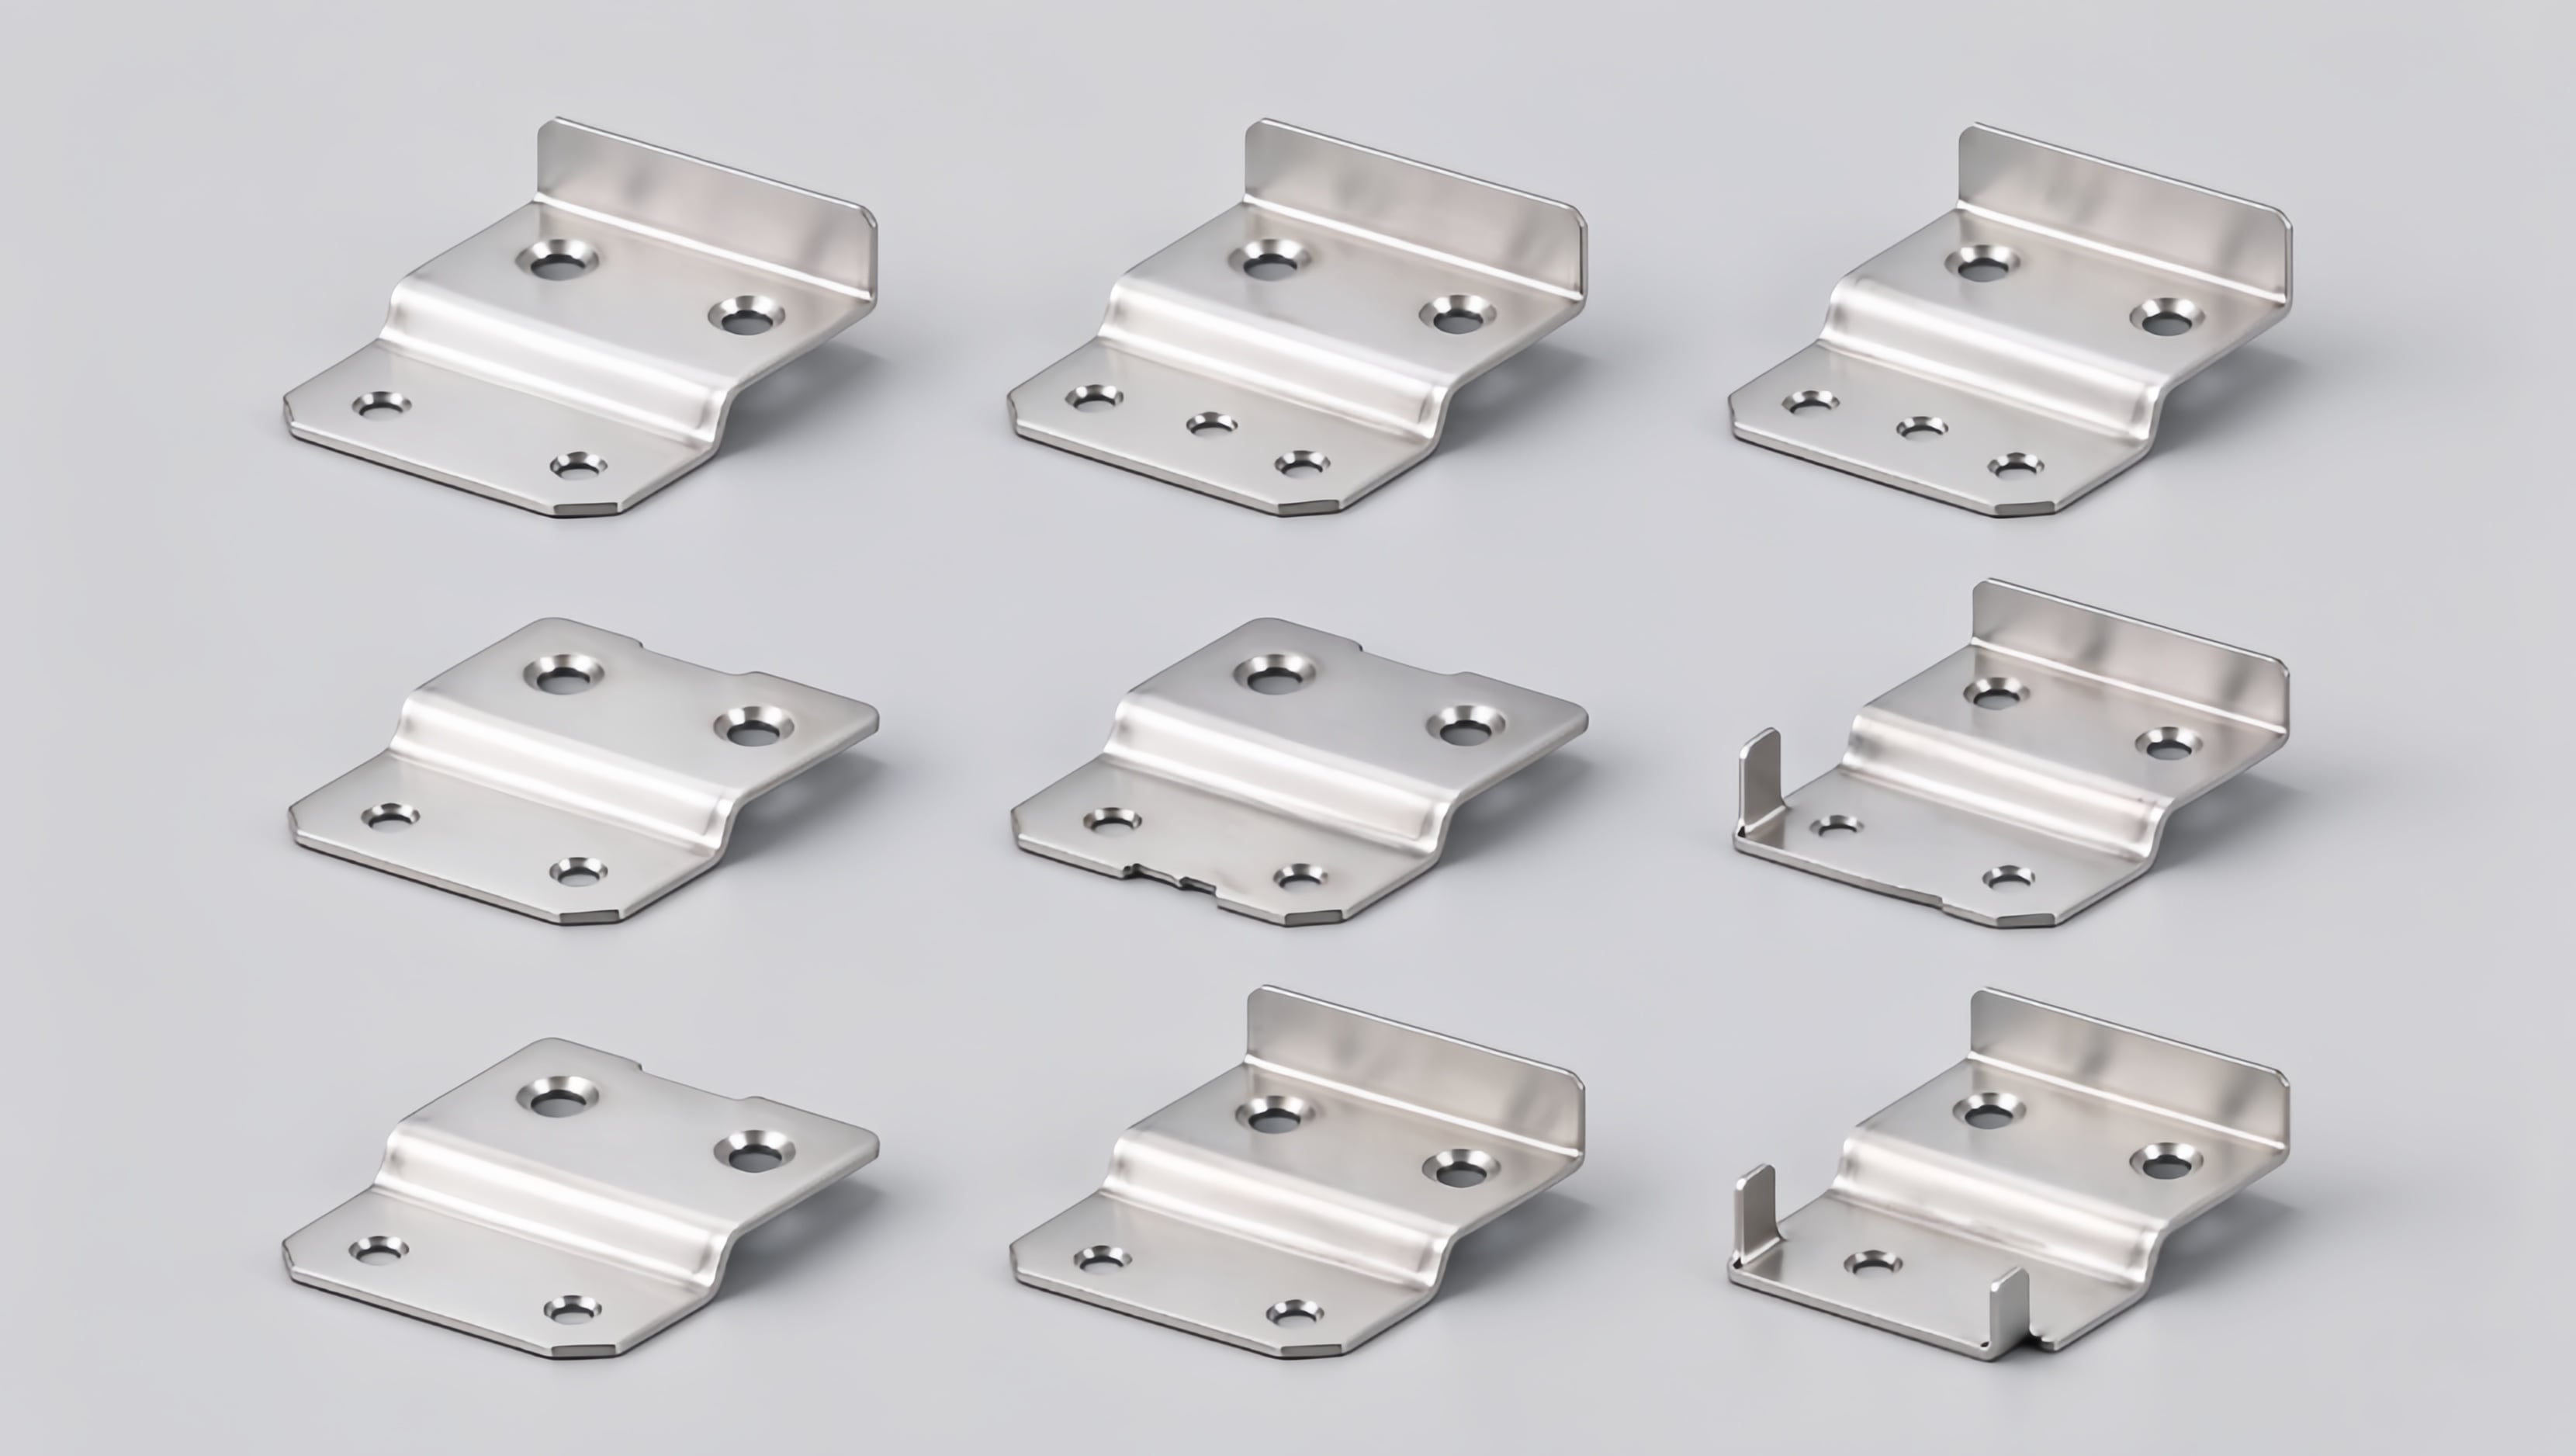
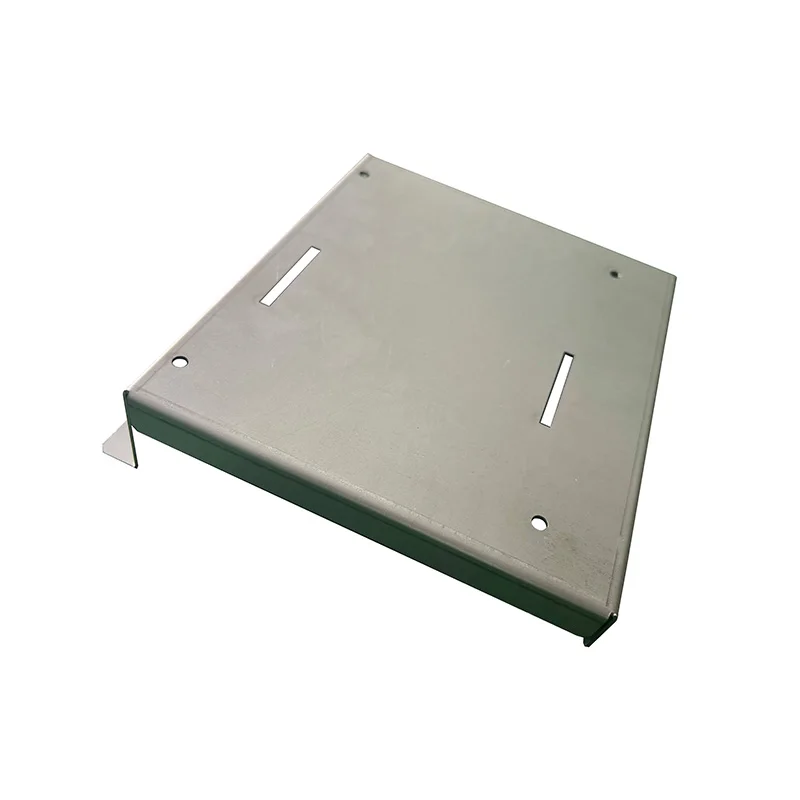
Custom SUS304 sensor mounting brackets 1.jpg
Custom SUS304 sensor mounting brackets produced by DEEPLINK progressive die stamping — one part replaces a four-piece welded assembly.

Quick Answer (30-Second Summary)

DEEPLINK moved a custom stainless steel (SUS304) sensor mounting bracket from engineering drawing to 20,000-piece mass production in 45 days, holding ±0.05 mm critical tolerances with a 99.6% first-pass yield — and cut the customer's unit cost by 28% by consolidating a four-piece welded sub-assembly into a single progressive die stamped part.

  • 8-station progressive die, designed and built in-house with carbide inserts and bending compensation.
  • 20,000 pcs delivered in 45 days, prototype to shipment (2 stamping lines, 110 strokes per minute).
  • ±0.05 mm on critical hole position, flatness 0.10 mm, burr < 0.05 mm; Cpk 1.6 verified by SPC.
  • PPAP Level 3 documentation, zero field failures after 12 months in service.

1. The Challenge: One Stamped Part Must Replace a Four-Piece Welded Assembly

A European industrial automation OEM was redesigning the mounting system of a new generation of position sensors used in washdown and high-vibration environments. The previous design was a four-piece welded assembly: two plates, one tube and a spacer, welded and then re-machined. It was expensive, heavy and suffered from weld distortion that shifted the sensor axis. The OEM's engineering team issued a clear brief for a redesign:

  • Produce the bracket as one stamped part in SUS304 stainless steel, 1.2 mm thick, with an integral 105° locating bend.
  • Hold ±0.05 mm on the two mounting-hole positions and ±0.10 mm flatness, with burr below 0.05 mm on all edges.
  • Withstand a 500 N static load and salt-spray exposure of 96 hours without red rust (neutral salt spray, ISO 9227).
  • Initial order of 20,000 pieces, with samples required within 3 weeks and full production within 7 weeks.
  • Submit PPAP Level 3 documentation before volume shipment.

The OEM had already failed with one supplier: hole positions drifted by ±0.15 mm during production, burrs damaged the sensor sealing lip during press-fit, and deliveries slipped twice. They needed a partner who could design the tooling, control the process and document everything — not just run a press.

Project Requirements at a Glance

Requirement Specification Verification Method
Material SUS304 stainless steel, 1.2 mm, mill certificate required Incoming material inspection + spectro analysis
Critical tolerance ±0.05 mm hole position; flatness 0.10 mm; burr < 0.05 mm FAI, CMM, GO/NO-GO gauges, CCD inline inspection
Mechanical 500 N static load; 105° bend angle with springback control Load test per batch; angle gauge per stroke check
Corrosion 96 h neutral salt spray, no red rust; RoHS & REACH Salt spray test (ISO 9227), material certs
Volume / lead time 20,000 pcs; samples ≤ 3 weeks; production ≤ 7 weeks Project schedule + PPAP gate review
Documentation PPAP Level 3 (PFMEA, control plan, MSA, Cpk ≥ 1.33) Customer approval at sample stage

2. Our Solution: DFM Review, In-House Tooling and a Progressive Die Built for Consistency

DEEPLINK's engineering team treated the project as a design-for-manufacturability (DFM) program, not a simple quote. Before cutting steel, we ran a strip-layout study with forming simulation to balance material utilization, bend compensation and die strength.

2.1 DFM Review and Strip Layout

  • Re-located the two mounting holes relative to the bend line to keep edge distances within safe limits and eliminate micro-cracking risk in SUS304.
  • Added a 0.4 mm overbend compensation so the 105° angle springs back to exactly 105° at 20°C.
  • Optimized nesting raised material utilization from 61% to 78%, directly reducing blank cost.
  • Recommended laser-cut prototype samples during die build so the customer could fit-test in the first week — we deliver these in as little as 3 days.

2.2 Eight-Station Progressive Die

We designed and built an 8-station progressive die in-house (our tooling shop supports quick-change inserts and in-die sensing):

  • Station layout: piloting → forming the locating bend (with overbend) → restrike for springback recovery → precision piercing of mounting holes → coining of the sealing face → trimming → cutoff.
  • Carbide (tungsten) inserts on piercing and forming stations for long tool life at 110 SPM.
  • Nitrogen die springs and a fixed-strip design that keeps strip position stable, eliminating hole-position drift between stations.
  • Tool steel certified and heat-treated in-house, with a documented die try-out and FAI before production release.
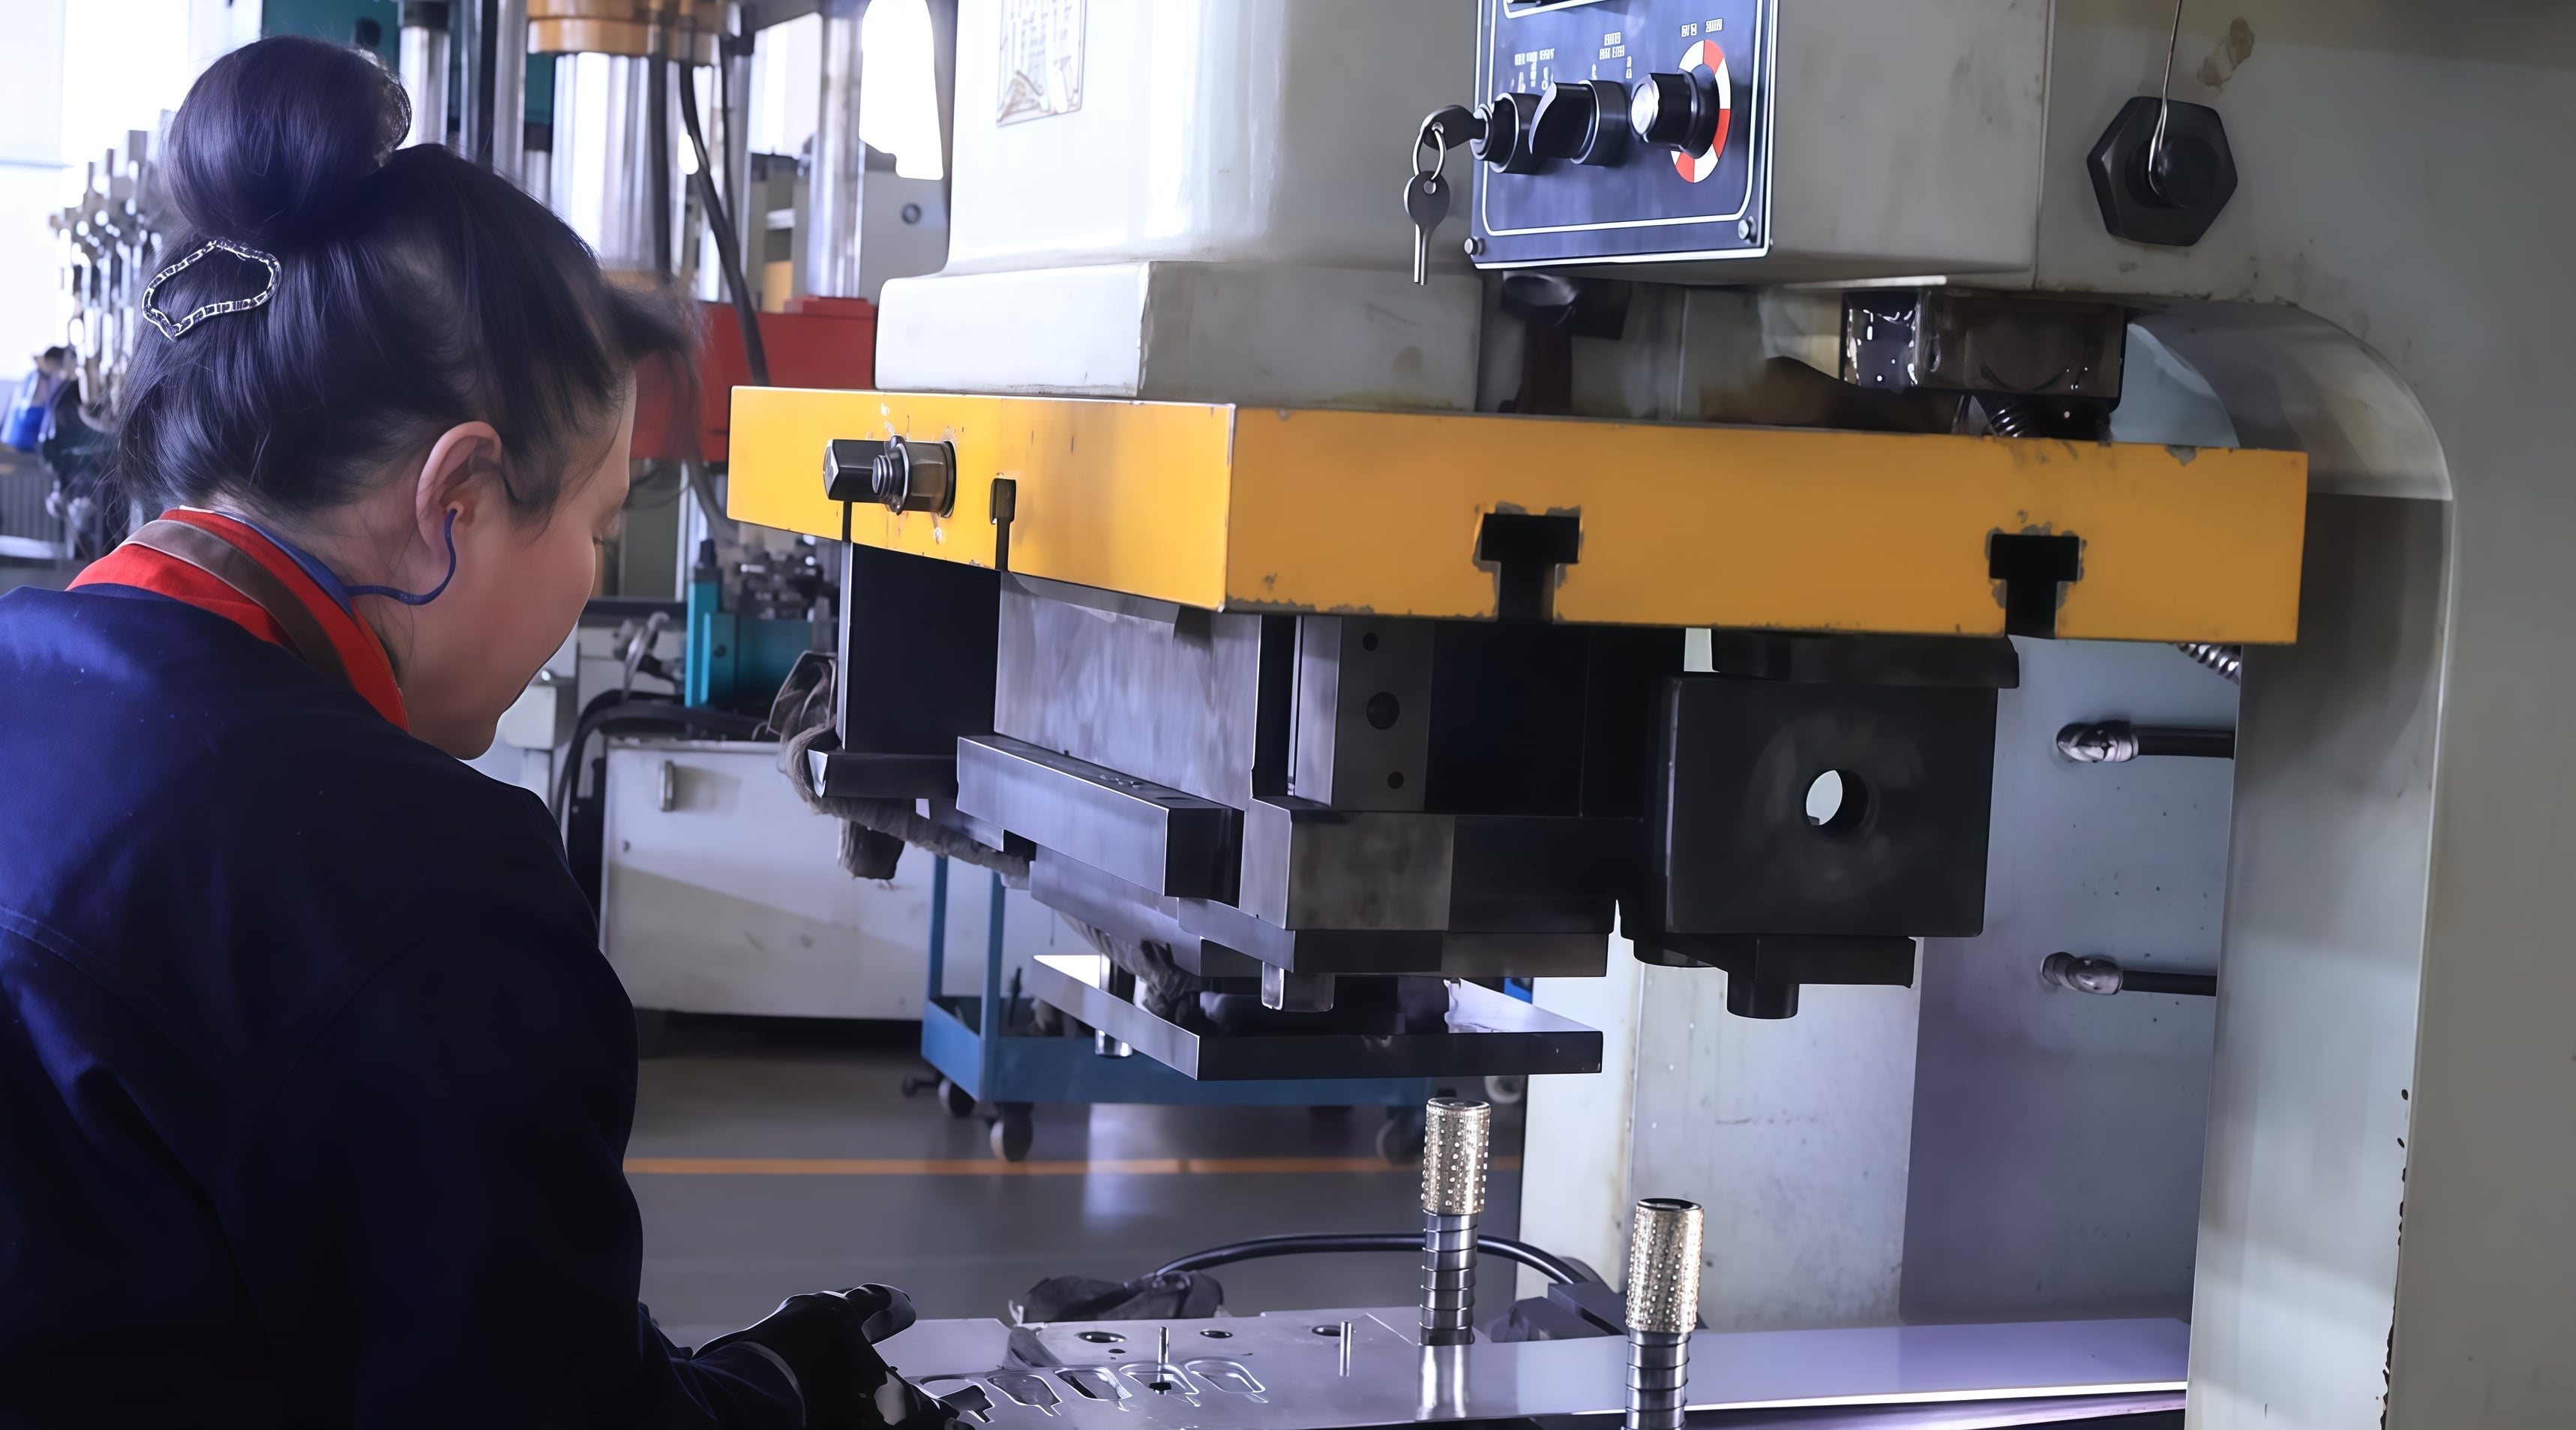
stamping 1.jpg
The 8-station progressive die runs the SUS304 coil at 110 strokes per minute across two automated stamping lines.

2.3 Surface Treatment and Compliance

After stamping, the brackets were electropolished and passivated to remove micro-burrs, brighten the surface and build a passive film that passed the 96-hour salt spray test. All consumables and coatings are RoHS and REACH compliant, supported by material and process certificates.

3. Project Timeline: From RFQ to 20,000 Pieces in 45 Days

Week 1
RFQ & DFM Review24-hour quotation response; strip-layout and tolerance feasibility study; material and coating confirmation.
Weeks 1–3
Die Design & Build8-station progressive die designed and built in-house; die try-out; laser-cut fit samples shipped for customer testing.
Week 3
Samples & FAIProduction samples from the actual die; full first article inspection (39+ checks per project) against the drawing.
Week 4
Customer Approval & PPAPCustomer fit-and-function sign-off; PPAP Level 3 file — PFMEA, control plan, MSA, Cpk 1.6.
Week 5
Pilot Run500-piece pilot; in-process SPC every 2 hours; dimensional data shared for customer review.
Weeks 6–7
Mass Production20,000 pieces across two stamping lines at 110 SPM; CCD inline inspection on hole position.
Week 8
QC, Packing & ShipmentFinal AQL inspection, salt-spray and load sampling, protective packing, full traceability documents shipped.

4. Quality Control: 39+ Checks per Project, From Material to Packing

Quality was managed as a closed loop under our ISO 9001 system, mirroring the four-stage control described in our metal stamping process guide:

  • Incoming material inspection — mill certificates, spectro analysis and surface checks before the coil enters the press.
  • First article inspection (FAI) — 39+ dimensional and visual checks per project on the CMM, verified against the customer drawing before batch release.
  • In-process control — SPC sampling every 2 hours, GO/NO-GO gauging, and inline CCD optical inspection on mounting-hole position, with automatic rejection of out-of-tolerance parts.
  • Final inspection & packaging — AQL sampling, 96-hour salt spray and 500 N load sampling per batch, then protective packing with lot traceability.
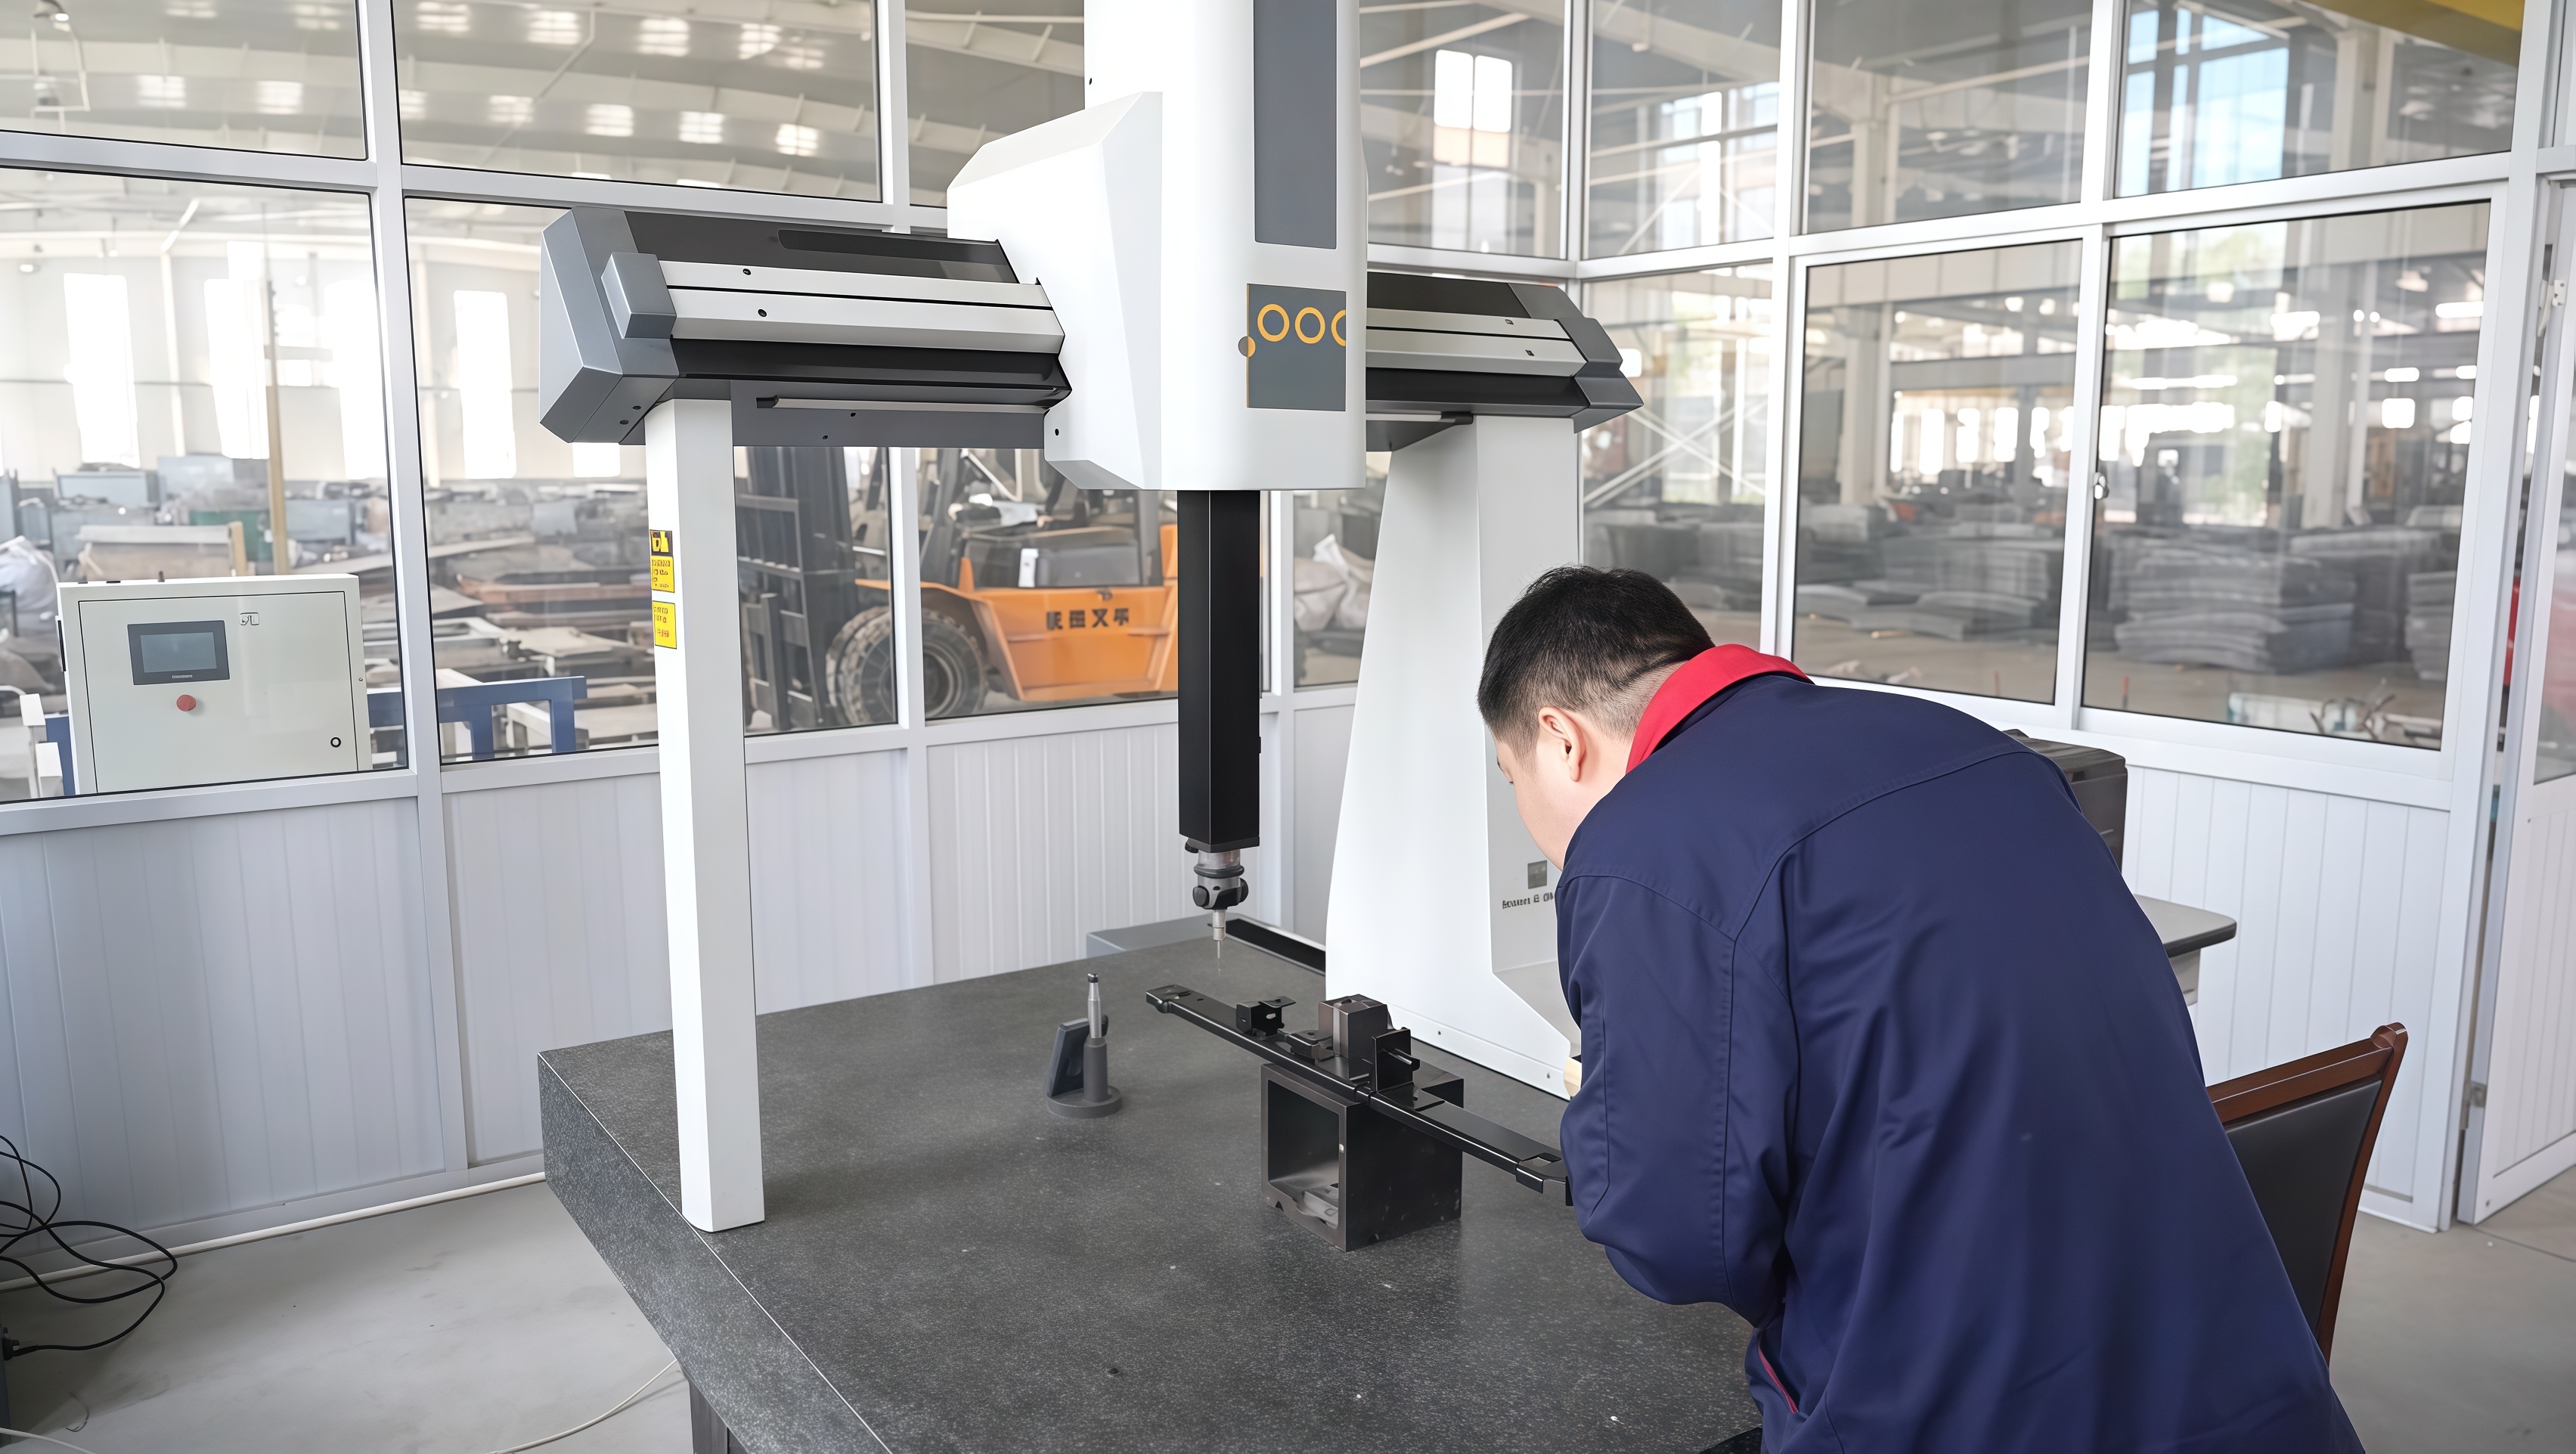
4.14独立站文章配图7.jpg
First article inspection on the CMM and digital calipers — every batch is verified against the drawing before release.

5. Results: Measurable Impact for the Customer

20,000 pcsDelivered on schedule in 45 days
±0.05 mmCritical tolerance held, Cpk 1.6
99.6%First-pass yield on the line
−28%Unit cost vs. welded assembly
78%Material utilization (was 61%)
110 SPMProduction speed, 2 lines
96 hSalt spray passed, zero red rust
0Field failures in 12 months

Target vs. Delivered

6. Why Global OEMs Choose DEEPLINK for Progressive Die Stamping

This project is typical of how we work, not an exception. As an ISO 9001 certified metal stamping factory with more than 5,000 square meters of workshop, 100+ staff and in-house tooling support, DEEPLINK brings three things that matter most on volume stamping programs:

For buyers comparing suppliers, we also cover the full process chain under one roof — laser cutting, custom metal stamping parts, sheet metal fabrication, CNC machining and welding — so follow-on operations never need a second vendor.

7. FAQ

What is progressive die stamping?
Progressive die stamping is a high-speed metal forming process in which a strip of metal passes through a multi-station die on a stamping press. Each press stroke performs a sequence of operations — piloting, blanking, piercing, bending, forming, trimming and cutoff — so a finished part exits at every stroke. It is the most cost-effective process for high-volume metal stamping parts with tight tolerances, which is why it is the backbone of automotive, electronics and appliance component production.
What tolerances can DEEPLINK hold on stamped parts?
DEEPLINK routinely holds ±0.05 mm on critical stamped dimensions such as hole position, and down to ±0.03 mm where die design and material allow. Flatness of 0.10 mm and burr control below 0.05 mm are standard, verified through first article inspection and in-process SPC. To understand how these numbers are achieved, see our guide to the factors affecting metal stamping precision.
What is the minimum order quantity for custom metal stamping?
DEEPLINK has no minimum order quantity. We support single-unit sample customization as well as mass production — the same engineering team handles prototype development and 20,000-piece (or larger) production runs, backed by OEM customization services.
How long does it take to get stamping samples and mass production?
Laser-cut prototype samples are typically delivered within 3 days. Progressive die build and production samples take 2–3 weeks, and standard mass production lead time is 7–15 days after sample approval. A complete DFM-to-delivery program of 20,000 pieces can be finished in about 45 days, as this case study shows.
Does DEEPLINK provide PPAP documentation?
Yes. DEEPLINK provides PPAP Level 3 documentation on request — PFMEA, control plan, MSA studies, dimensional reports and material certificates — plus documented inspection and traceability from incoming material to final packing under our ISO 9001 quality system.
What surface treatments are available for stamped parts?
DEEPLINK offers electropolishing, passivation, anodizing, powder coating, zinc and nickel plating, galvanizing and sandblasting, all RoHS and REACH compliant. Treatments are matched to the operating environment — this project used electropolishing and passivation to pass a 96-hour salt spray test in a washdown application.
Have a drawing? Let's review it within 24 hours.

Free DFM analysis and quotation — no minimum order quantity, samples from 3 days.

Get a Quote for Your Stamping Project

Prev

OEM Case Study: Precision Custom Sheet Metal Enclosures for Electronic Equipment

ALL

Red Powder-Coated Deep-Drawn Steel Tank with Threaded Outlet — OEM Case Study

Next
Recommended Products